China Shaving Foam Manufacturer Quality Checklist for International Buyers
2026-09-06
Every year, thousands of international buyers source shaving foam from China, but only a few end up with a manufacturer they actually reorder from. Why? Because they skip the quality checklist that separates a reliable partner from a shipment of leaky cans. At Wilson, we’ve audited dozens of production lines and reviewed hundreds of test reports, so we know exactly where corners get cut. In this post, we’re sharing the non-negotiable checks—from foam density and pH to canister pressure and regulatory paperwork—that you should demand before signing any contract.
Ingredient Traceability Before You Sign Anything
A supplier's polished spec sheet won't tell you whether the turmeric in that blend actually came from the farm they named. Traceability means being able to follow each ingredient back through every handler, processor, and storage point—and if that chain has gaps, you inherit them the moment you sign. Ask for batch-level records, not just annual audits or a certificate of analysis for one sample. If a vendor hesitates to share supplier names, country of origin, or handling dates, treat that hesitation as a data point.
Before the contract locks you in, run a traceability test on a single ingredient from the formula. Request the lot number, then have them walk you back to the raw material receipt. You're checking whether the paperwork matches physical reality, and whether recalls could be narrowed to a specific batch or would force a sprawling withdrawal. Contracts should also spell out how quickly traceability records must be delivered during a safety event—72 hours is common, but some vendors quietly default to 'as available.' If that clause is missing or vague, negotiating it later costs more than fixing it now.
The Filling Line Audit Most Buyers Skip
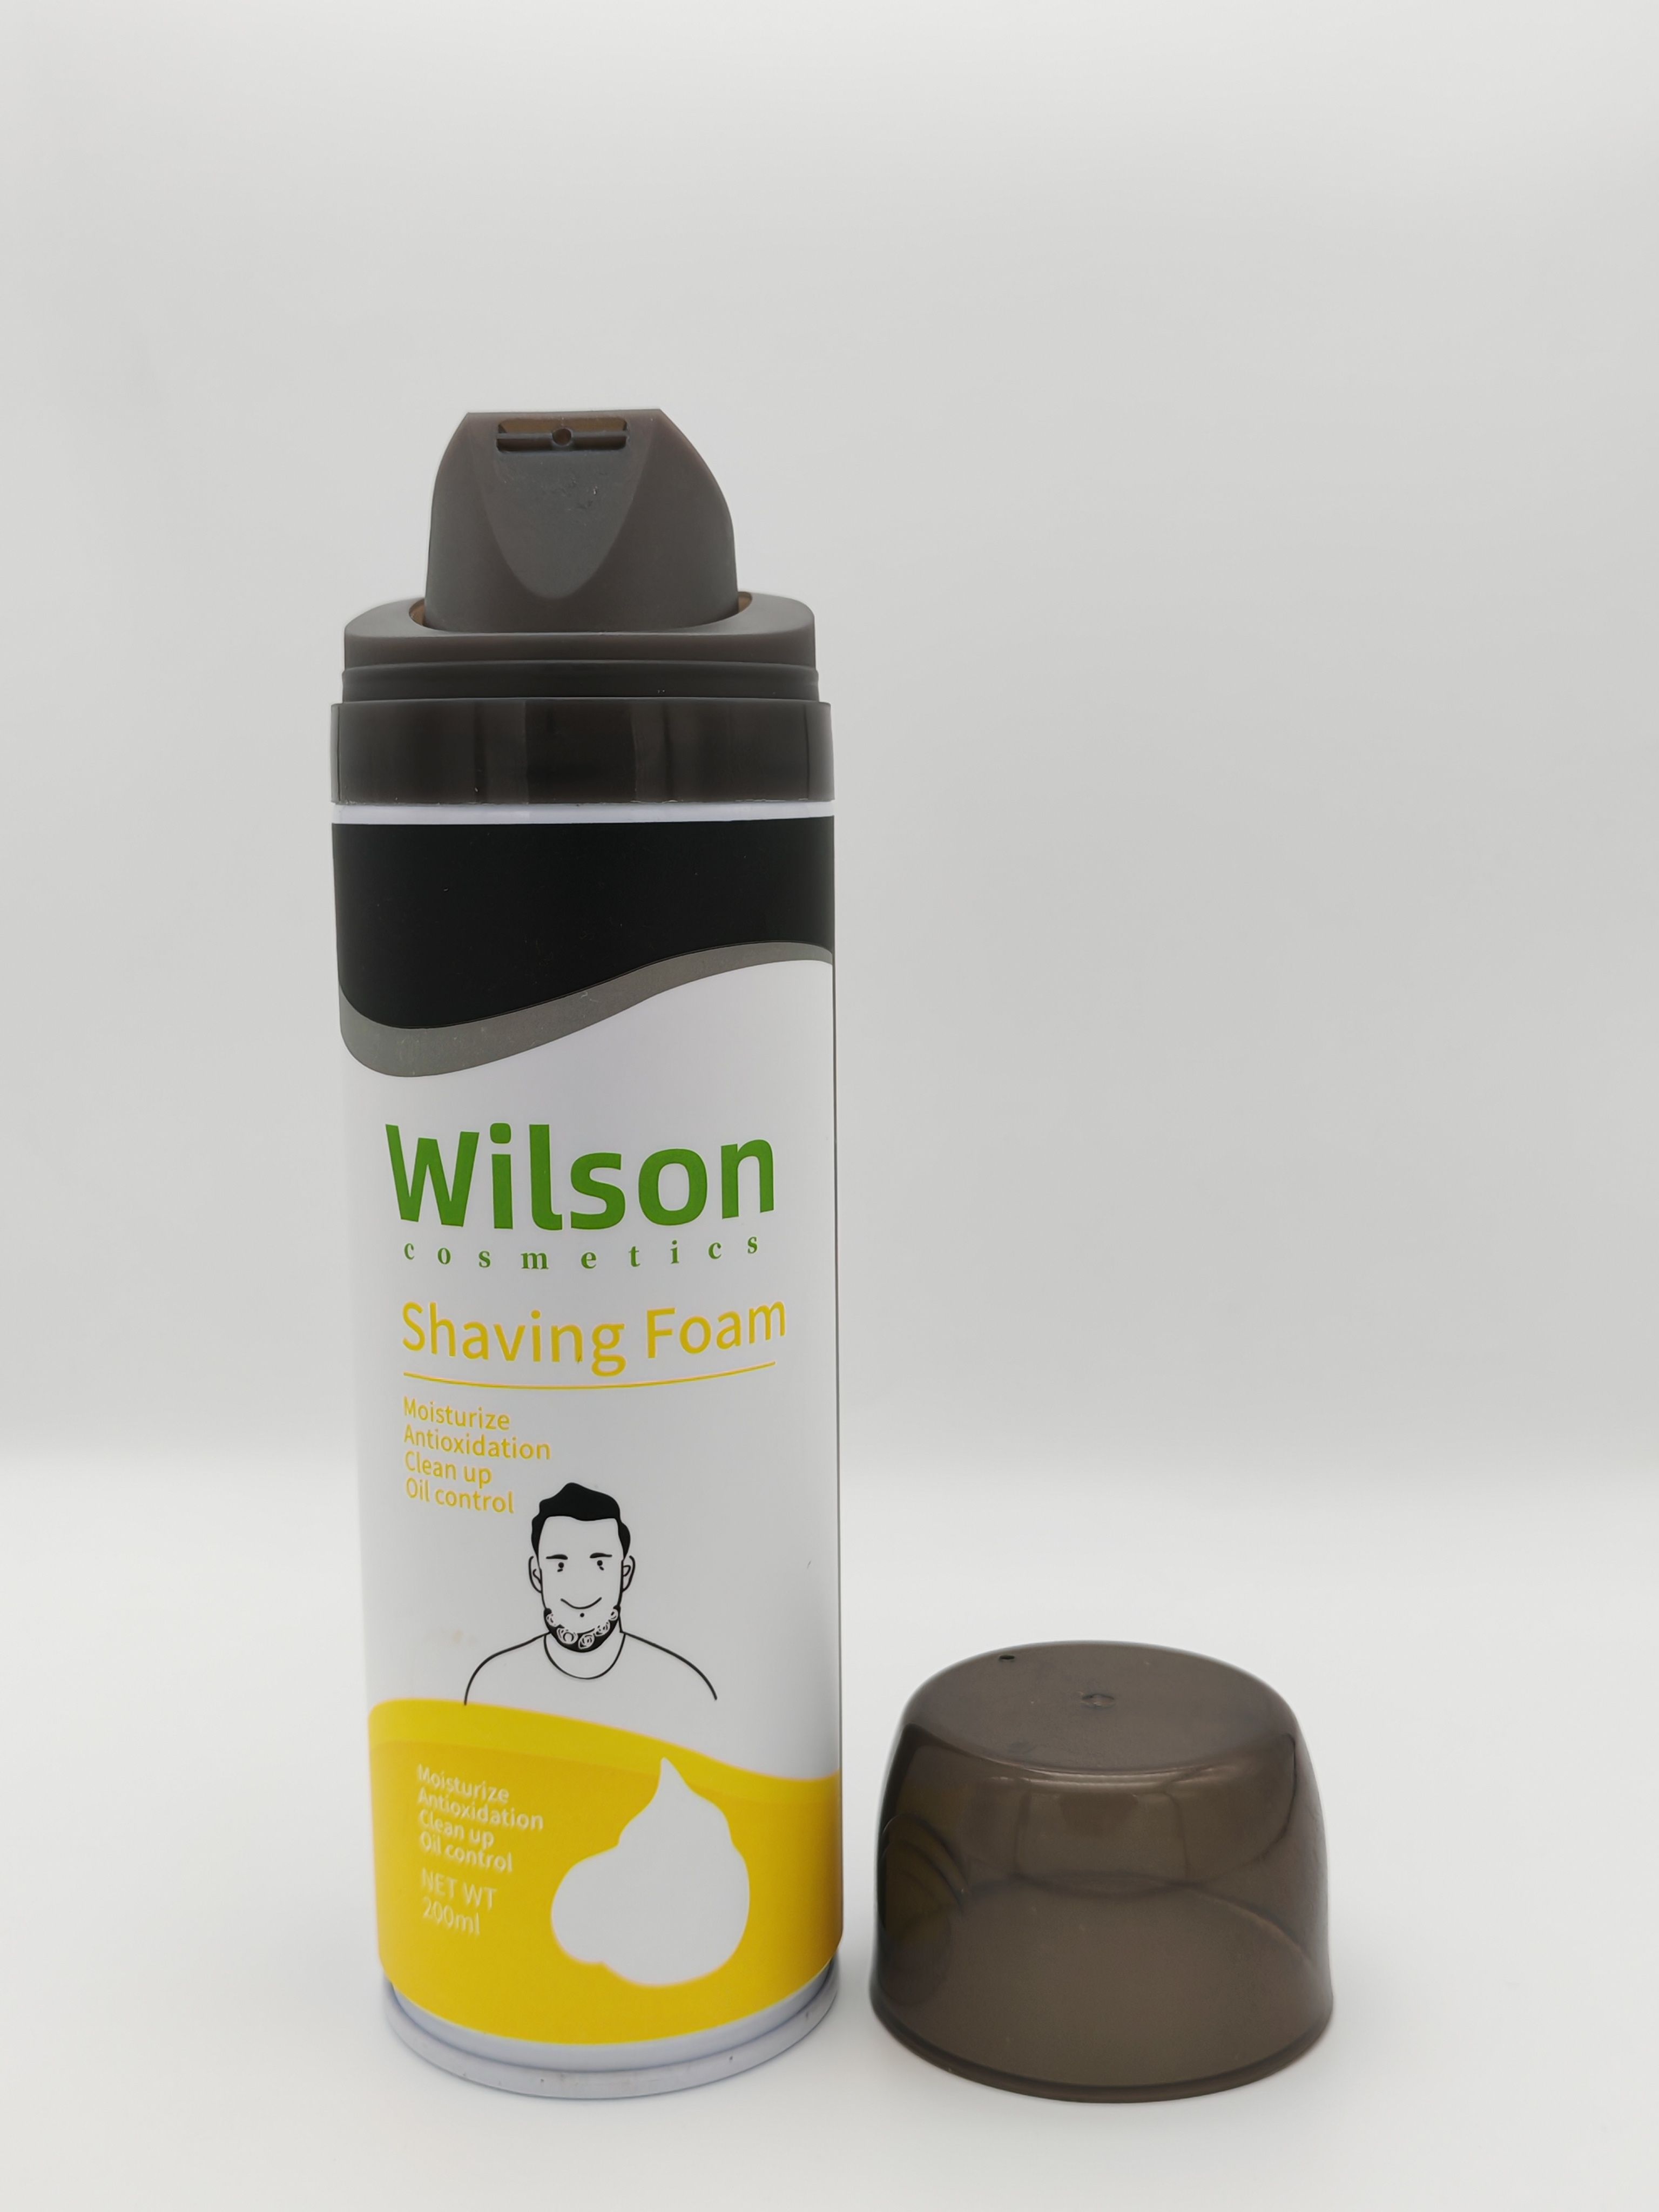
Most procurement teams treat a filling line purchase like any other equipment buy—they compare spec sheets, negotiate price, and maybe watch a demo. But the actual line audit, the kind where you walk the floor of a running facility and watch the machine handle real product, often gets skipped. Buyers assume that if the specs match and the demo looks smooth, the line will perform. That assumption has cost companies thousands of hours in downtime and rework when the equipment hits their own plant floor and encounters variables no demo ever simulated.
A proper filling line audit goes beyond checking boxes. It means running your actual container, your actual product viscosity, and your actual closure through the line at production speed. It means watching how the filler handles foam, splashing, or particulates. It means checking clean-in-place access points, changeover times, and whether the conveyor integration matches your existing setup. Skipping this step is like buying a car without taking it on the highway—you might discover the steering pulls only after you've signed the papers.
The buyers who do insist on a thorough audit rarely regret it. They catch issues like inconsistent fill levels at high speed, seal failures with certain cap lots, or bottlenecks at the infeed that no CAD drawing would reveal. More importantly, they build leverage into the negotiation—once a vendor knows you're serious about verifying performance under real conditions, the conversation shifts from price haggling to performance guarantees. That shift is what separates a smart capital investment from a very expensive paperweight.
Can the Foam Survive a Tropical Shipping Container
The question isn't just about temperature; it's about the combined assault of heat, humidity, and time. A steel shipping container crossing the tropics can easily reach internal temperatures above 60°C (140°F), with relative humidity near saturation once the doors are sealed and any residual moisture in the cargo or air gets trapped. For many foam types, especially ester-based polyurethane, that environment triggers hydrolysis—a chemical reaction where water molecules break the polymer chains. The foam loses tensile strength, becomes brittle, and can develop a sour, musty smell that never really goes away.
Ether-based polyurethane foams handle moisture better, but they aren't immune. Prolonged exposure to high heat accelerates oxidation, which yellows the foam and makes it crumble at the edges. The real difference between a foam that survives and one that doesn't often comes down to additives. Anti-hydrolysis agents, antioxidants, and even a small percentage of biocides can dramatically extend the foam's life inside a container. Packaging plays an equally important role: sealing foam in vapor-barrier bags with desiccant packs, or choosing a container with a white-painted roof and shaded stowage, can reduce the peak temperature by several degrees.
Accelerated aging tests give a rough picture of what happens during a three-week voyage. A foam sample held at 70°C and 95% relative humidity for 14 days may lose 30–50% of its original tensile strength if it has no stabilization. That's why many manufacturers have quietly shifted to polyether-based formulations or added carbodiimide stabilizers to ester foams. Without those changes, the foam may arrive looking fine but fail soon after—collapsed cushions, brittle padding, or a residue of dust that makes customers think the product was defective from the start.
Leak and Corrosion Checks That Predict Returns
Facilities that treat leak and corrosion monitoring as a routine chore miss the real opportunity. The data from these checks, when tracked over time and matched against equipment performance, starts to reveal patterns that directly tie to revenue. A pump that loses just 3% of its seal integrity month over month isn't just a maintenance issue; it's an early signal of upcoming unplanned downtime, which usually costs more than the repair itself. Teams that act on those subtle changes before they become visible failures consistently avoid the expensive emergency fixes that eat into margins.
The trick is to stop looking at corrosion as a single event and start reading it as a story. Wall thickness measurements taken at the same spot, season after season, show whether a vessel is degrading slowly or about to give way. When that trend is compared with production output, a clear link emerges: units running at higher temperatures or pressures tend to corrode faster, and their output drops slightly before any leak appears. Spotting that downward turn early lets operators adjust run rates or swap out a section during planned maintenance, keeping the line profitable instead of idle.
What many overlook is that leak and corrosion checks don't just prevent losses; they also reveal where extra production capacity is hiding. A reactor that shows minimal wear after years of service can often be pushed harder than its original design limits suggest, while one that's degrading quickly should be throttled back. Using inspection data to make those calls turns a compliance task into a direct driver of return on assets.
Paperwork Depth for Batch Records and COAs
The real depth in batch records shows up in the unglamorous details—operator initials next to every critical step, timestamps for pH adjustments, and a clear chain from raw material lot numbers to final released batch. For a typical API or finished drug, a single batch record can run thirty to sixty pages, but the page count alone means little. What matters is that a reviewer can reconstruct exactly what happened on the floor without asking the operator. A well-built record includes not just expected readings but also space for unexpected observations, and any deviation is described with enough context to understand whether it was a one-off or part of a trend.
COAs, by contrast, are meant to be concise—usually one or two pages—but their depth lies in the assumptions behind each result. A robust COA doesn't just list "conforms"; it references the specific test method version, the acceptance criteria, and the actual numerical result where applicable. For high-risk products, some customers expect the COA to tie back to the batch record through a unique identifier, so that a single result can be traced to the exact instrument, column, or analyst who generated it. This cross-referencing is what separates a checklist-style certificate from a document that can stand up in an audit.
The right paperwork depth is product-risk dependent. A simple excipient may only need a two-page batch record and a one-page COA, while a sterile injectable or a controlled substance will carry far more granular documentation—including environmental monitoring data, filter integrity test results, and a full reconciliation of labels and packaging. Over-documenting every minor step can bury critical information, but under-documenting leaves gaps that regulators or customers will eventually find. The goal is not to produce the thickest binder, but to make every page earn its place.
Factory Floor Signals a Checklist Cannot Capture
A checklist is built from what has already gone wrong or what an engineer thought to ask about. On the factory floor, the earliest warnings rarely fit those boxes. A slight change in the pitch of a spindle, a pause in a worker’s hand before loading a part, the faint scent of overheated insulation near a panel—these signals exist long before a parameter drifts out of range. They are not items to tick off because they have no stable label yet.
Experienced operators often act on these impressions without being able to explain them in the moment. After thousands of cycles, they know the normal rhythm of the line the way a musician knows when an instrument is slightly out of tune. A checklist demands explicit, yes-or-no answers, but the floor speaks in degrees and textures. That mismatch means the most useful information can be filtered out precisely because it does not fit the format.
Relying on the checklist alone creates a false sense of coverage. It documents what was known yesterday, not what is beginning to fail today. The signals that matter on a factory floor are often weak and ambiguous: a vibration felt through the soles of the feet, a change in how a conveyor accelerates. They ask for attention rather than confirmation, and they disappear when everyone is waiting for a box to turn red.
FAQ
Ask for a sample batch from the actual production line rather than a hand-picked lab sample. Review the full ingredient disclosure against EU or ASEAN cosmetic regulations, and confirm the propellant type. A surprising number of issues stem from cheap propellant blends that affect foam density and skin feel.
Request third-party test reports for skin irritation, ocular irritation, and microbial limits from labs like SGS, Intertek, or TÜV. Also ask for a certificate of analysis for each batch, not just a one-time type test. Some manufacturers will share patch test results from dermatology panels; that's a good sign, but always cross-check the lab's accreditation.
At minimum, look for ISO 22716 (cosmetic GMP). If you sell in the EU, the manufacturer should have a Responsible Person arrangement and be familiar with CPNP notification. For US-bound goods, FDA VCRP registration helps but isn't a quality mark. Also check if the facility holds any cruelty-free or vegan certifications if that's part of your brand promise.
Accelerated stability testing at 40°C and 75% humidity for three months, plus freeze-thaw cycles. The foam should maintain its expansion ratio and drainage time within set specs. Also run a canister pressure test and a spray pattern test under different temperatures. If the manufacturer can't provide these, walk away.
Ask for the IFRA certificate for the fragrance compound and confirm the preservative system is within Annex V limits if shipping to the EU. Have the manufacturer run a repeated insult patch test (RIPT) on the final formula. A manufacturer that only offers a single fragrance option and claims it's hypoallergenic without test data is a warning sign.
Check that the can lining is epoxy or polymer coated to resist corrosion from the alkaline soap base. Verify the valve and actuator compatibility with the foam expansion rate—some cheap valves clog with stearate-rich formulas. Labeling must include ingredient INCI names, net weight, batch code, and any required hazard symbols for the propellant.
Request a traceability matrix that maps each ingredient to its supplier and batch. Visit the warehouse unannounced if possible and look for expired stearic acid or triethanolamine. Ask about their policy on heavy metals and 1,4-dioxane in surfactants. Some manufacturers blend cheap industrial-grade TEA that can raise nitrosamine levels; a reputable one will share residual solvent reports.
They quote a price 30% below other audited suppliers, refuse to share the full ingredient list until after deposit, or push you to accept their in-house lab reports only. Also watch for vague answers about propellant purity, no documented change control for formula tweaks, and a sample turnaround time that's suspiciously fast—that often means no real stability check.
Conclusion
Before you place a purchase order with any shaving foam maker in China, push hard on traceability at the ingredient level. A supplier name on a certificate is not enough; you need to see lot-specific records for surfactants, propellants, and preservatives, including incoming QC release data. Once that clears, look at the filling line itself. Many buyers review final samples but never watch how the can is gassed and crimped. Ask for fill weight and pressure charts across a full production shift, not just a golden batch. Then ask the harder question: can the foam survive a tropical shipping container? If the product sits for four weeks at 50 degrees Celsius with high humidity, does it still deliver a stable lather without propellant loss or separation? A manufacturer that cannot show a passing accelerated transport test is a risk you are importing by the pallet.
Leak and corrosion failures often show up months later as customer returns. A quick water bath check is not enough. You want pressure decay testing on finished cans and corrosion coupon data for the can body, valve, and seam using your actual formula. Paperwork matters just as much. Real batch records should show deviations, line stoppages, and rework, not a clean template. Certificates of analysis need actual measured values, not repeated spec limits. Finally, walk the factory floor yourself. Look at how raw materials are quarantined, whether gauges have calibration stickers within date, and whether operators record data in real time or fill in logs at the end of shift. Those small signals tell you more about batch consistency than any polished audit report.
Contact Us
Contact Person: Simon
Email: [email protected]
Tel/WhatsApp: +86 13267966849
Website: https://www.wilsoncosmetic.com