Custom Shot Blasting Machine Factory Insights for Superior Surface Preparation
2026-11-02
If you’ve ever watched a coating fail early because the blast profile was too shallow, you already know why equipment choice matters. At PuHua, a custom shot blasting machine factory, we don’t just assemble cabinets—we engineer the wheel, abrasive flow, and dust collection around your specific part geometry. This article shares the factory-floor criteria we use to turn surface preparation from a guess into a controlled process. From choosing between wheel and air blast to tuning reclaim systems, you’ll get a practical look at what separates a machine that barely works from one that delivers repeatable anchor profiles. Ready to see inside the build?
Tailoring Blast Patterns to Odd Geometries
Odd geometries show up in almost every real blast site, from a wedge of ore pinching out against waste rock to a basement excavation wrapped around existing footings. Square or rectangular patterns assume a clean free face and uniform burden, but corners, narrow necks, and curved boundaries break that assumption fast. The practical fix is to read the shape first and then shift hole spacing, angle, and charge weight accordingly instead of forcing a standard grid onto it.
In tight corners or sharply tapering sections, the rock tends to clamp harder, so reducing burden and using lighter charges keeps fragmentation even without sending flyrock into the next lot. Wider pockets can handle slightly larger spacing, but only if the delay timing is adjusted so each hole breaks toward the nearest free face rather than fighting the geometry. Electronic detonators make this kind of fine-tuning much easier than trying to force pyrotechnic caps into a fixed sequence.
Buffer holes and pre-splitting become more than afterthoughts when the boundary is irregular. A row of smaller, closely spaced holes along a jagged perimeter creates a cleaner separation line and protects the final wall from overbreak. On sites where the odd geometry includes unexpected voids or backfilled zones, drilling extra probe holes helps map the actual burden before loading, so the blast pattern can be adjusted on the fly instead of relying on a plan drawn from outdated survey data.
Inside the Test Bay Where Air Pressure and Abrasive Flow Get Dialed In
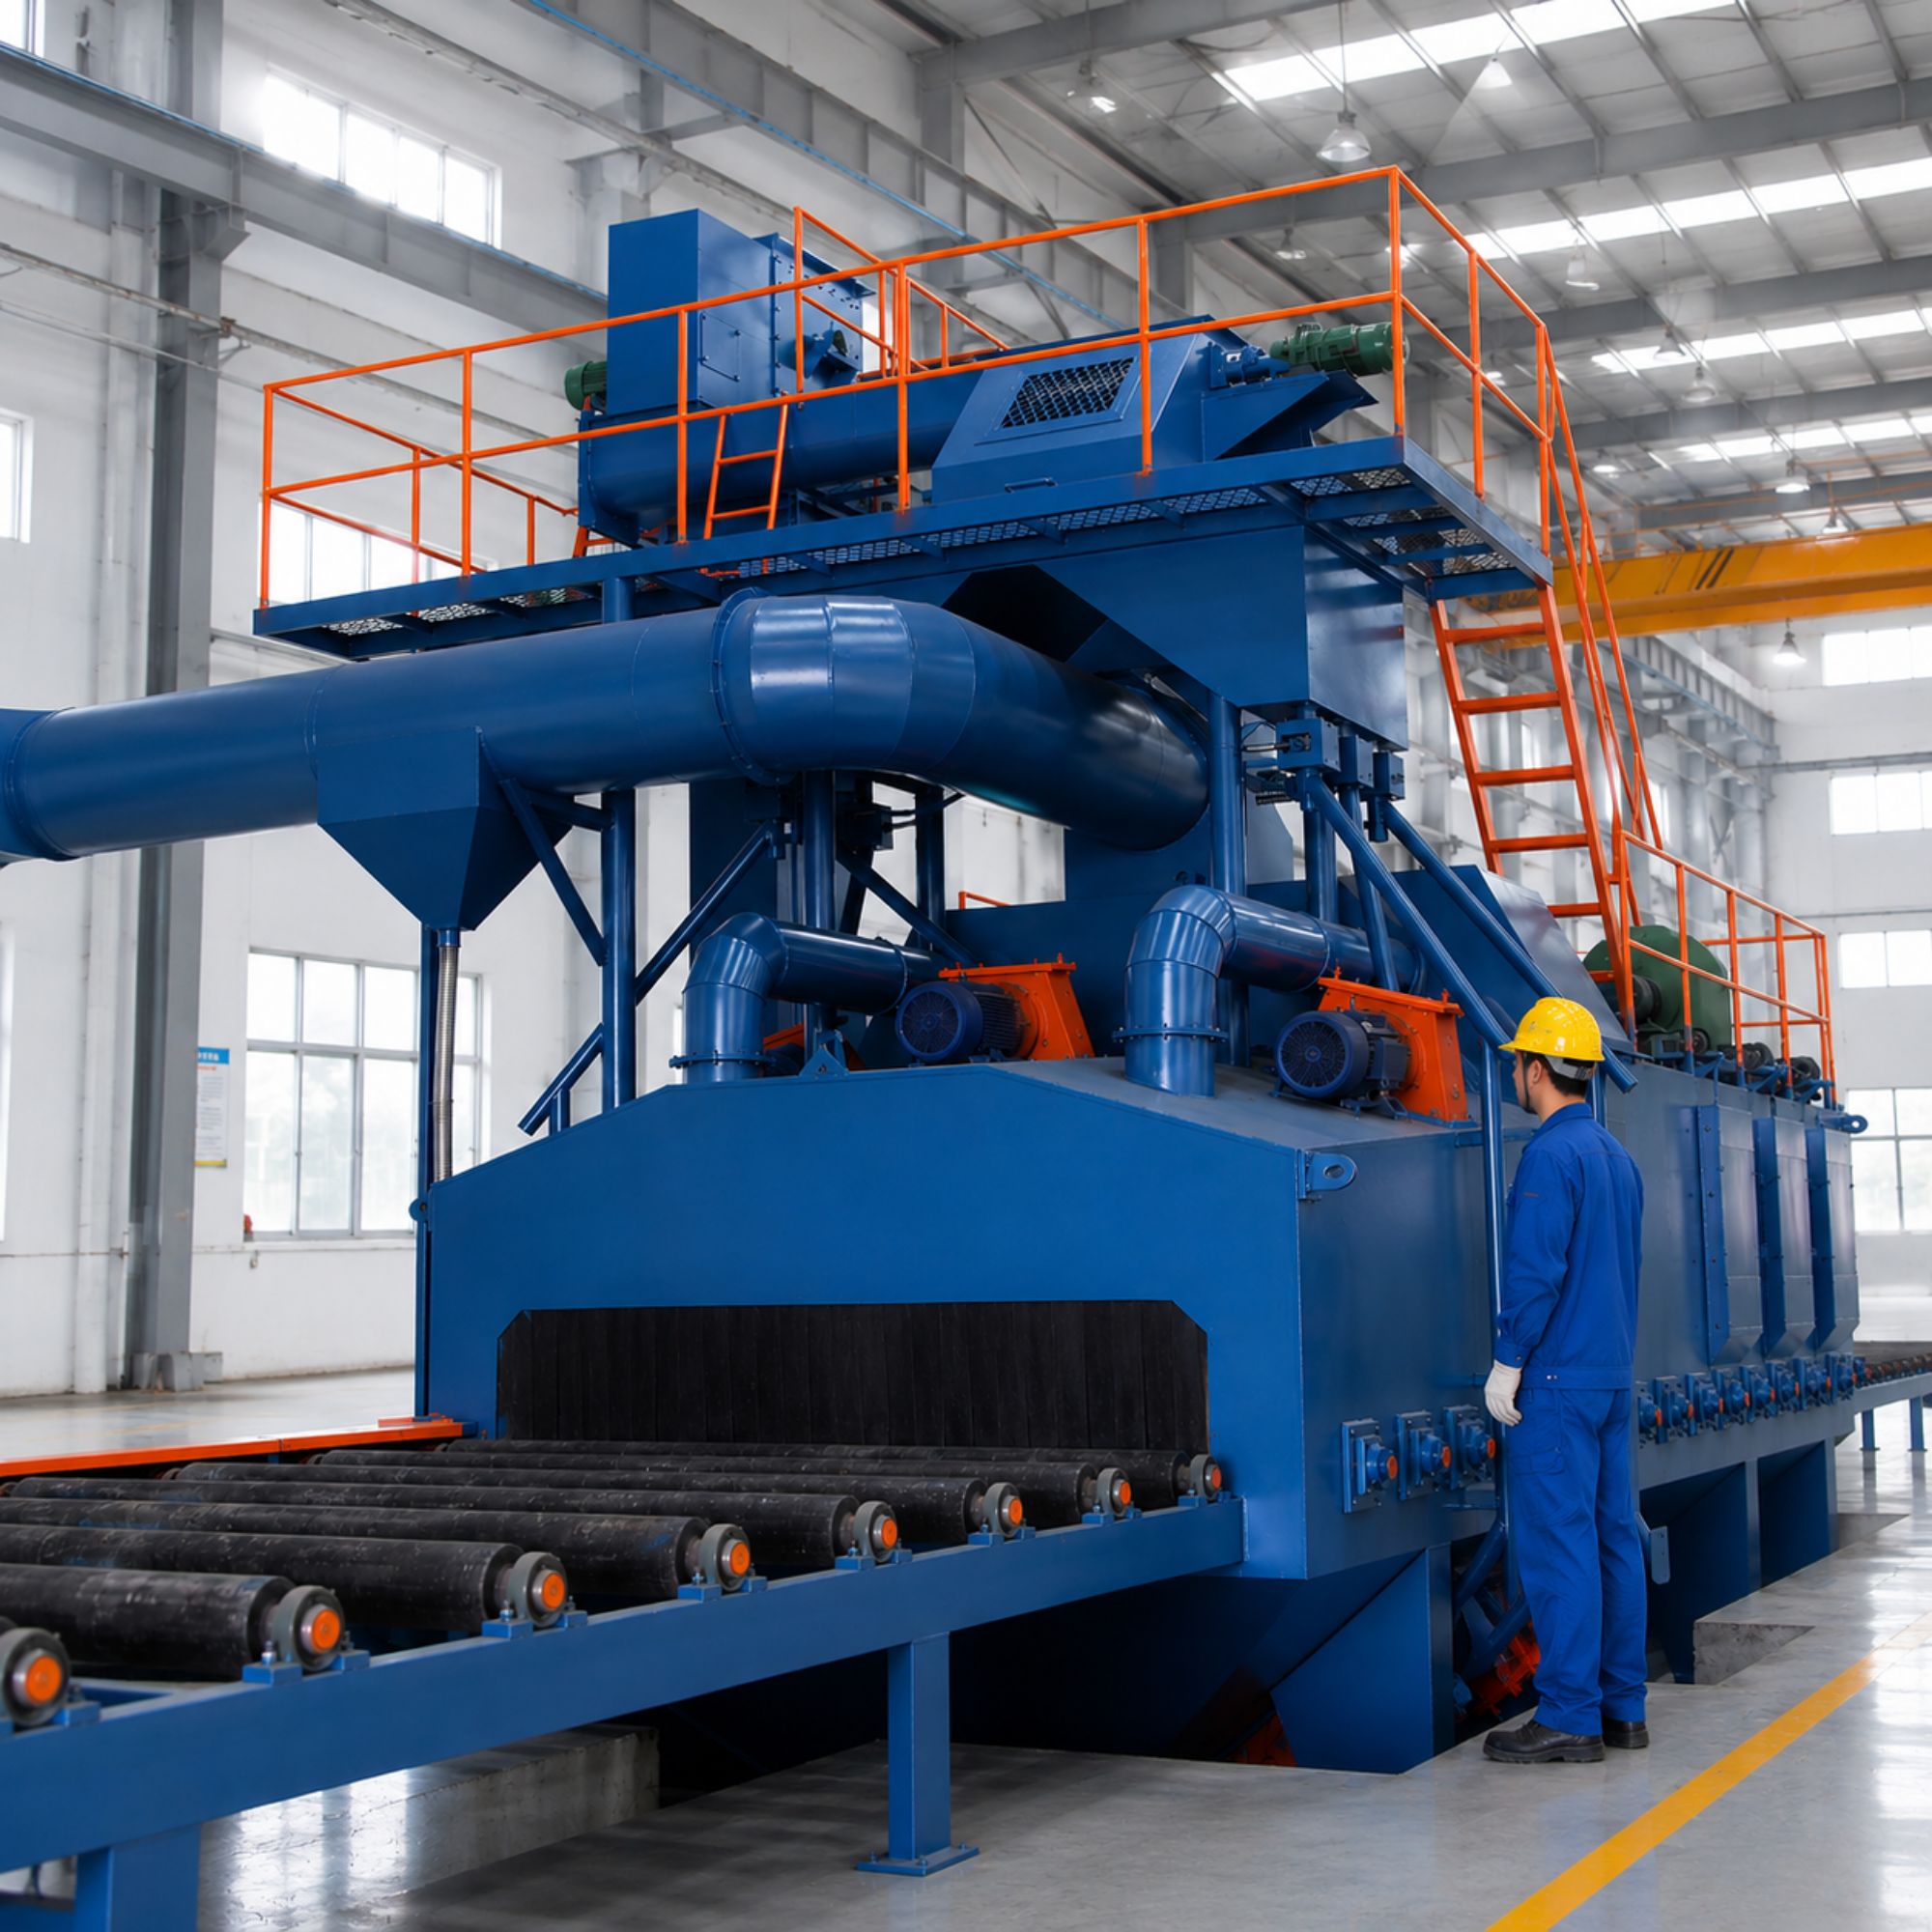
The test bay smells of fine grit and machine oil the moment the door swings shut. Along one wall, a bank of analog pressure gauges trembles as compressed air pushes through a web of braided lines. A technician thumbs the regulator in quarter-turn increments, watching the needle settle before reaching for the abrasive metering valve. Here, the mix is never guessed—it is weighed, bounced, and observed through a small sight glass until the stream runs dense but not choked.
Abrasive flow is dialed in by feel more than formula. When the blast nozzle opens, the hiss changes pitch if the grit ratio drifts too lean; too rich and the hose kicks like a garden snake. The crew keeps a logbook taped to the control panel with handwritten notes like “minus two percent on garnet, nozzle wear even.” Small adjustments happen between runs, not after them, because every test piece that leaves the bay carries the signature of those quiet corrections.
Why Your Surface Finish Spec Dictates the Grit, Not the Other Way Around
Many shops still reach for a familiar grit first and then measure to see where the surface landed. That sequence quietly puts the cart before the horse. A surface finish callout on a print—whether Ra, Rz, or a specific microinch value—is a functional requirement tied to sealing, wear, coating adhesion, or even appearance. Letting a habit-driven grit choice override that target means you are optimizing the process for convenience rather than the part’s actual job.
The practical reason to start from the spec is that identical grits do not produce identical finishes across materials and equipment. A P400 abrasive on 6061 aluminum might yield a smoother Ra than the same P400 on 304 stainless, simply because of differences in hardness, cutting action, and loading. If you routinely default to P320 for every “smooth” surface, you’ll end up over-processing some parts and under-processing others. Working backward from the required finish—say, selecting a starting grit to remove tool marks, then stepping down based on measured roughness—keeps the process predictable.
This is not about following a rule for its own sake. When a finish spec dictates the grit sequence, you stop guessing. You can hold a 32 microinch Ra consistently on a milled aluminum housing by planning the abrasive steps after the required value, not by discovering later that the chosen belt left deep scratches. The finish is the deliverable; the grit is just the tool to get there.
Engineering Out Dust, Noise, and Wear on the Factory Floor
A factory floor is a living system of moving parts, and the constant battle against dust, noise, and mechanical wear often dictates how smoothly it runs. Dust settles into bearings, coats sensors, and works its way into pneumatic lines until precision starts to fade. Noise isn't just an annoyance—it's wasted energy, loose fittings, and misalignment announcing themselves before a failure shows up. Wear is the slow creep of friction, vibration, and heat that gradually robs machines of their tolerances. Treating these three as separate problems means chasing symptoms forever; the smarter approach is to design them out at the source.
Dust control starts with containment and active extraction, not just more frequent cleaning. Enclosing transfer points, using negative-pressure hoods over conveyors, and switching from compressed-air blow-off to vacuum systems can cut airborne particles by half or more. For noise, the quick wins are often overlooked: balancing rotating parts, replacing worn sprockets before they rattle, and using isolation mounts on vibrating screens. But the bigger payoff comes from rethinking the process itself—substituting impact-free conveyance for drop chutes, or slowspeed, high-torque motors for high-speed fans. Wear reduction follows the same logic: hardened inserts on highabrasion surfaces, automatic lubrication that matches load cycles, and alignment protocols that keep shafts true instead of waiting for catastrophic runout.
What separates a durable floor from one that constantly needs intervention is the habit of measuring the invisible. Vibration analysis on gearboxes, oil particulate counts, and acoustic mapping during normal operation create a baseline that reveals drift long before a breakdown. Dust accumulation rates tell you where seals are failing; noise frequency shifts point to loosening fasteners; wear particle shapes identify whether it's cutting, sliding, or fatigue. None of this requires a smart factory or a big budget—just a handheld meter, a consistent routine, and the will to act on early warnings. The result is a floor where the air stays clearer, the hum stays steady, and the equipment ages like a well-maintained engine instead of grinding itself into scrap.
Reading Surface Profiles Before the Coating Ever Touches Metal
A blast-cleaned steel panel can look uniform to the naked eye and still be completely wrong for the coating you're about to apply. The peaks and valleys left by abrasive leave a fingerprint that coating adhesion depends on, yet too often it's treated as a box-ticking exercise. Measuring the profile before any primer or topcoat goes down is not about collecting a number—it's about knowing whether the surface will hold under stress, flex, and years of exposure. Replica tape, stylus instruments, and digital depth micrometers all tell slightly different stories, and trusting one without understanding its limits invites failure later.
The practical approach starts with a simple question: what does this coating actually need? A thin-film epoxy wants a crisp, angular profile in a specific range, while a high-build polyurethane might forgive a coarser texture. Taking three or five readings across the same surface often reveals more than a single average ever will, because blast patterns shift with nozzle wear, air pressure, and operator rhythm. When the profile reads too low in a corner or near a weld seam, that's a signal to adjust technique before the coating ever touches metal—cheap insurance compared to a field failure investigation.
Smart inspectors also pair profile numbers with visual references and a quick tactile check. A profile that measures within spec but has rounded, peened peaks will behave differently from one with sharp, fractured edges, even if the micrometer says they're identical. Documenting the method, the location of each reading, and any deviation from the expected range turns a routine check into traceable evidence. By reading the surface this carefully before coating, you stop guessing about adhesion and start controlling it.
What a Factory Walkthrough Reveals About Build Quality
A walkthrough tells you more than a spec sheet ever will. Watch how a chassis moves down the line and you'll see whether torque tools are calibrated daily or left to drift. The quiet stations—where workers check thread engagement or wipe down mating surfaces—often matter more than the loud, photogenic automation.
Small details compound. At one plant, every wiring harness was routed through a plastic comb before the dash went in, eliminating the kind of chafe that only shows up after 50,000 miles. Another builder insisted on hand-starting every bolt before a power tool touched it. That's the difference between a vehicle that feels tight at delivery and one that stays tight.
None of this shows up on a brochure. It comes from walking the line, asking operators what they'd change, and seeing whether rejects are displayed as trophies or hidden in a corner. A factory that treats assembly as an engineering problem, not just a cost center, builds quality you can't fake.
FAQ
A custom unit is built around your workpiece geometry, production volume, and required surface profile. For instance, if you handle long steel beams, we would adjust the cabinet length, blast wheel positioning, and material handling to avoid dead zones, something off-the-shelf equipment rarely addresses well.
It depends on the base metal, desired roughness, and whether you are removing mill scale, rust, or old coatings. For delicate aluminum parts, we might use glass beads at lower pressure; for heavy steel plates, steel grit gives a sharper anchor profile for later coating adhesion.
We often work with structural steel fabricators, automotive component suppliers, foundries, and pipe coating plants. Each has unique constraints, like cycle time in automotive or dust control in food-grade stainless steel finishing, so the machine layout and filtration system get tailored accordingly.
Yes, that is actually one of the main reasons customers come to us. We map out the current conveyor speeds, load/unload points, and available floor space. Then we design the blast chamber and separator to match that flow, often adding automated loaders or turnover mechanisms to reduce manual handling.
We can reach Sa 2.5 or Sa 3 cleanliness levels for steel, with consistent roughness values like 50 to 100 microns Rz depending on the abrasive mix. The key is controlling the blast pattern and abrasive recycling so the profile stays uniform across large surfaces.
Every machine includes a high-efficiency cyclone separator and cartridge filter system sized to the blasting volume. For abrasive recovery, we use a combination of screw conveyors and bucket elevators. This keeps the working environment clean and reduces abrasive consumption by up to 30 percent compared to basic systems.
Basic details help a lot: the material and dimensions of your workpieces, current surface condition, target surface profile or coating spec, hourly throughput, and any space limitations. Even rough sketches or photos of the parts let us propose the right blast wheel count and power.
Typically 10 to 14 weeks from design freeze to shipment, depending on complexity and current workload. We prioritize the mechanical design review with your team to avoid later changes. Installation and commissioning usually take another week or two, including operator training.
Conclusion
Walk into any custom shot blasting machine factory and the first thing that stands out is how much attention goes into shape. Tailoring blast patterns to odd geometries isn't a feature—it's the baseline. A casting with deep recesses, a weldment with sharp inside corners, or a thin-walled extrusion all demand nozzle angles, wheel positions, and oscillation speeds that off-the-shelf equipment can't touch. In the test bay, technicians run sample parts with adjustable air pressure and abrasive flow, making small changes until the blast envelope wraps every surface uniformly. That tuning process often surprises buyers who assume a bigger machine solves everything. But the real leverage comes from reversing the usual logic: your surface finish spec dictates the grit, not the other way around. If a coating requires a 2.5 mil angular profile, the abrasive size, hardness, and velocity have to be selected backward from that requirement—not from what's sitting in the hopper.
A factory walkthrough reveals build quality in details that a brochure never shows. Look for sealed bearing housings, abrasion-resistant liners with quick-release clamps, and dust collection ducting that isn't an afterthought. Engineering out dust, noise, and wear on the factory floor means the machine should run quieter than the conveyor feeding it, with negative pressure at every loading point so fine particulates stay inside the blast zone. After processing, the real test happens before coating ever touches metal: technicians read surface profiles with replica tape, profilometers, or digital roughness gauges. They check not just average roughness but peak count and angularity, because a smooth-looking profile can still fail adhesion under thermal cycling. When you see that level of verification built into the factory's routine, it's a sign that the company treats surface preparation as a measurable process rather than a cosmetic step.
Contact Us
Contact Person: Bruce
Email: [email protected]
Tel/WhatsApp: +86 15166629468
Website: https://www.povalchina.com/