Gold Plating Production Line Solutions to Optimize Quality and Throughput
2026-08-28
What if the key to better gold plating isn't choosing between speed and quality, but rethinking how they work together? Many lines still treat throughput and finish consistency as competing priorities, leading to costly trade-offs. Yet optimized production line solutions are changing that calculus. From advanced rectification and agitation control to real-time bath analytics, the right configuration can lift both metrics simultaneously. At Junda, we've seen how tailored line design turns this challenge into a measurable advantage. In this article, we'll break down the strategies that matter most.
Dialing In Additive Levels Without the Guesswork
Most shops still treat additive dosing like a kitchen recipe—a splash of this, a pinch of that—then wonder why the final product drifts. The real problem isn't the additive itself; it's relying on memory and habit instead of a repeatable procedure. Once you accept that guessing is the enemy, you can start building a method that removes it entirely.
Start by measuring the baseline: run a small, controlled batch with no additive and record the exact performance gap you're trying to close. Then introduce the additive in fixed increments—say 0.5% by weight—and test each step under identical conditions. Keep a simple log with timestamps, ambient temperature, and any visual or mechanical changes. After three or four iterations, you'll see a clear response curve instead of a fuzzy feeling.
The payoff comes when a batch falls out of spec and you don't have to guess what changed. You can trace back to the last known good setting and adjust by a defined amount. Over time, you'll develop a narrow working window for each material and process, which means less waste, fewer rejected parts, and a team that trusts the numbers more than someone's intuition.
Rack Design That Keeps Current Flowing Where It Counts
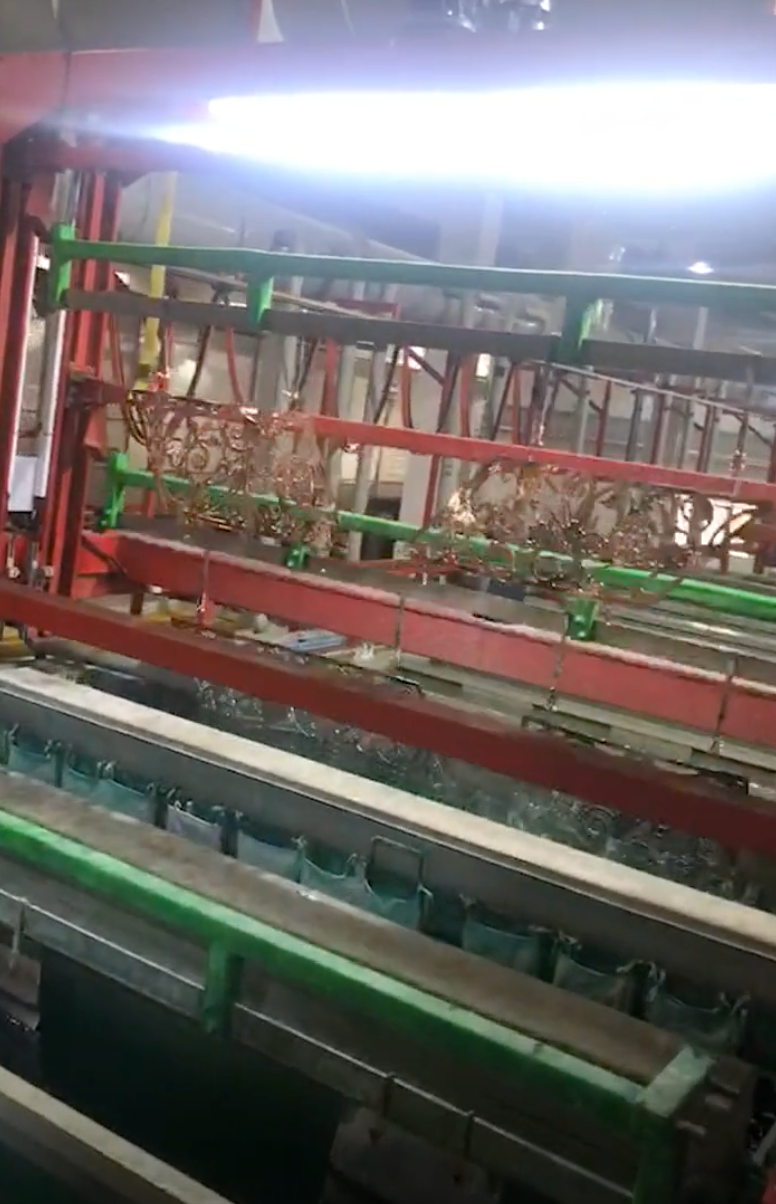
In a high-density rack, power delivery is only as good as the path from busbar to blade. Clever rack designs shorten that path with vertical busbars that run behind the mounting rails, minimizing resistance and heat buildup. This keeps voltage stable even when every slot is populated with GPUs or storage arrays.
The best designs also account for failure without interrupting service. Dual redundant power feeds, separated by physical barriers inside the rack frame, let one side carry the full load while the other is serviced. Hot-swappable power distribution units snap into place without tools, so a failing module never turns into a full rack outage.
Attention to materials matters more than most people realize. Tin-plated copper busbars with thick cross-sections reduce contact resistance at connection points, while louvered side panels create a natural chimney effect for passive cooling. These small choices add up, ensuring current reaches the processors instead of turning into wasted heat.
Why Your Conveyor Speed Is Sabotaging Plating Thickness
In many plating lines, conveyor speed is treated as a throughput setting rather than a process variable. That’s a mistake. The speed sets how long each part remains in the plating bath, and this residence time directly controls how much metal deposits. Increase the speed and the cathode has less time to attract ions from the solution, so the coating comes out thin even if the rectifier settings stay the same.
What often gets overlooked is speed fluctuation. A worn chain, a slipping drive, or even slight load changes can create small variations in line speed. Those variations translate into uneven thickness across a rack or between successive racks. You might see acceptable average thickness on a test coupon, yet still end up with thin edges or shadowed areas that fail salt spray or adhesion tests. By the time that happens, most people start adjusting chemistry or anode placement—when the real culprit is inconsistent part travel through the tank.
The most practical way to diagnose this is to log actual line speed for a full shift and compare it with thickness data from multiple locations on the same rack. If thickness swings correlate with speed changes, slow the conveyor until the spread tightens. A reduction of just 5–10% often brings thickness variation back into spec without any chemical changes. Keep in mind that current density, bath temperature, and speed are linked; changing speed may require a small adjustment in rectifier output, but first isolate speed to see its real impact.
Automation That Reads the Tank, Not Just the Timer
Most automated systems still run on a dumb timer, switching pumps or valves on and off at fixed intervals regardless of what's actually happening inside the tank. That means a pump might kick in when the tank is already full, wasting energy, or worse, it might stay off while the tank runs dry. Liquid levels don't follow a clock—demand spikes, weather changes, and refill rates drift. A timer can't see any of that, so it ends up being a crude guess that either overworks the equipment or leaves it vulnerable.
Automation that reads the tank changes the game by using level sensors—ultrasonic, pressure, or float switches—to measure the real amount of liquid at any moment. The controller then makes decisions based on that live data: a sump pump only kicks in when water actually hits a set threshold, not because it's 2 a.m. A chemical feed system stops dosing when the tank drops below a safe line. This isn't just smarter; it's cheaper to run, prevents dry running, and keeps gear from wearing out prematurely. It's the difference between following a blind schedule and actually paying attention to what the tank is telling you.
Inspection Points That Catch Trouble Before It Escapes
Early warning signs often hide in routine checks. A slight temperature rise, a faint vibration change, or an unusual noise can signal wear long before a breakdown. Documenting baseline readings for critical equipment gives you a reference point for spotting these deviations quickly.
Focus on high-stress areas: seals, fasteners, electrical connections, and fluid levels. A loose bolt on a rotating assembly may seem minor, but under load it can shift alignment and accelerate wear. Check torque marks, color changes on wiring, and moisture accumulation around connectors.
Trust your senses but back them with data. Use thermal imaging for hotspots, ultrasonic tools for leaks, and simple visual checks for cracks or corrosion. The goal is not to find problems after they appear, but to catch the subtle shifts that predict them.
Scheduled Shutdowns That Strengthen Your Throughput
A scheduled shutdown flips the usual script: instead of reacting to slowdowns after they hit, you choose the moment and the conditions. During those windows, teams rebuild primary indexes, drain stuck connection pools, and replace degraded drives before any of them turn into a hard failure. The result is not just avoided downtime—it's a system that moves data with fewer internal stops.
There is also a compounding effect that rarely shows up in a change log. When a shutdown is planned, the work is sequenced and rehearsed, so the actual outage shrinks over time. Each cycle removes the small frictions that accumulate under continuous load, giving you back memory, file handles, and CPU cycles that were previously wasted on recovery attempts.
FAQ
Check the rectifier output before touching the bath. Ripple or unstable current is the hidden cause of more thickness variation than most people expect. After that, verify the gold concentration with a quick titration, because a drop of just 0.5 g/L can shift deposition rates noticeably on high-volume lines.
Add a static rinse or reclaim tank right after the plating cell and hold parts over the bath for a couple extra seconds before they move. Slower withdrawal speeds and redesigned drain holes on barrels or racks also make a bigger difference than you might think. Recovering that dragged-out gold usually pays for the extra tank within months.
Almost always it is local current density running too high because the cathode masking is off or the anode is too close to a feature. Lower the voltage, use pulse plating, or add a thief shield to pull excess current away from edges. If the roughness shows up everywhere, check the filtration and look for suspended solids in the bath.
Adhesion failures that appear batch-by-batch usually point to upstream cleaning or activation inconsistencies rather than the gold bath itself. Look at the time between final rinse and plating, the age of the acid activation bath, and whether the nickel underplate is fully covering the base metal. A quick surface energy test on incoming parts can catch residue before it becomes a scrap issue.
If your weekly output is consistently above roughly 5000 to 8000 parts and you are running the same or similar part families, automation usually starts paying back in labor and rework reduction. But for high mix and short runs, a flexible batch line with better scheduling often beats a rigid automatic line because changeover time kills throughput.
Increase anode-to-cathode distance if you have tank space, and add auxiliary anodes or shielding around high-current-density zones. Using eductor agitation instead of air sparging helps force fresh solution into recesses. For really difficult geometries, pulse reverse plating can smooth out the distribution without sacrificing overall plating speed.
Run a small Hull cell panel once or twice per shift and compare it against a reference panel. It gives you a fast visual snapshot of brightness, burning, and throwing power for a few cents per test. Pair that with a simple daily check of pH, temperature, and gold concentration, and you will catch most problems before they affect production parts.
Don't just crank current density; instead improve agitation and use a more efficient anode arrangement so you can raise speed without causing burning or porosity. In many acid gold baths, staying near the middle of the recommended current density range and increasing agitation gives better overall throughput than running at the maximum with poor solution movement.
Conclusion
Fine-tuning additive levels no longer relies on trial and error. Real-time chemical analysis feeds exact replenishment rates back to dosing pumps, keeping brighteners and grain refiners within a narrow window that prevents dull patches or brittle deposits. Meanwhile, rack design gets a hard look: replacing worn contacts and balancing current distribution across every part eliminates the hidden voltage drops that cause uneven thickness on high-density loads. Conveyor speed is no longer set once and forgotten—engineers tie line speed to amperage density and bath temperature, so parts spend precisely the right dwell time in each cell instead of rushing through and starving the deposit.
Automation now reads the tank itself, not just elapsed time. Sensors track metal concentration, pH drift, and agitation flow, triggering adjustments mid-cycle rather than after a reject shows up at final inspection. Those inspection points have shifted upstream too: laser profilometry and X-ray fluorescence catch thickness deviation and porosity right after plating, long before parts reach assembly. Even scheduled shutdowns are reframed as throughput levers—planned anode replacement, filtration media swaps, and rectifier calibration during brief line stops prevent the unpredictable breakdowns that used to erase a week of production. The result is a line that holds tighter tolerances, runs longer between failures, and pushes more good parts out the door per shift.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com