Hard Endoscope Cleaning Brush: Inside a Top China Factory’s Precision Manufacturing Process
2026-06-08
Ever wondered what goes into making the hard endoscope cleaning brushes that ensure flawless hygiene in critical medical procedures? Step inside a leading Chinese factory where precision engineering meets rigorous quality control. From raw material selection to final inspection, every stage of the manufacturing process is designed to deliver reliability and performance. At the heart of this operation is KLDZS, a brand synonymous with excellence in brush technology. Discover how their meticulous craftsmanship sets a new standard for endoscope reprocessing.
Sourcing Medical-Grade Materials for Lasting Performance
Every component that goes into medical equipment leaves a mark on its overall lifecycle. We start by tracing materials back to their origin, assessing not just the purity certifications but the consistency of the supply chain. A resin might pass USP Class VI tests on paper, but if its viscosity swings between batches, the molding process suffers. Real reliability comes from suppliers who can provide decades of traceable data, not a single certificate.
Durability in clinical settings doesn't just mean surviving autoclave cycles. It means resisting the slow creep of iodine stains, the microcracks from hundreds of wipe-downs with aggressive disinfectants, and the constant ultraviolet exposure under surgical lights. We often find that material datasheets miss these real-world interactions entirely. That's why we run accelerated aging tests that simulate years of service in a matter of weeks, measuring the subtle shifts in impact resistance and color stability that dictate when a device actually gets retired.
Pushing beyond the conventional grades sometimes reveals unexpected options. For instance, a compounded silicone originally developed for aerospace seals might cut particulate shedding in a peristaltic pump by a significant margin. The key is partnering with material engineers who are willing to tweak formulations—adjusting a filler percentage or curing agent ratio—until the final part maintains its mechanical properties without compromise, year after year under load.
Micron-Level Precision in Bristle Cutting and Shaping
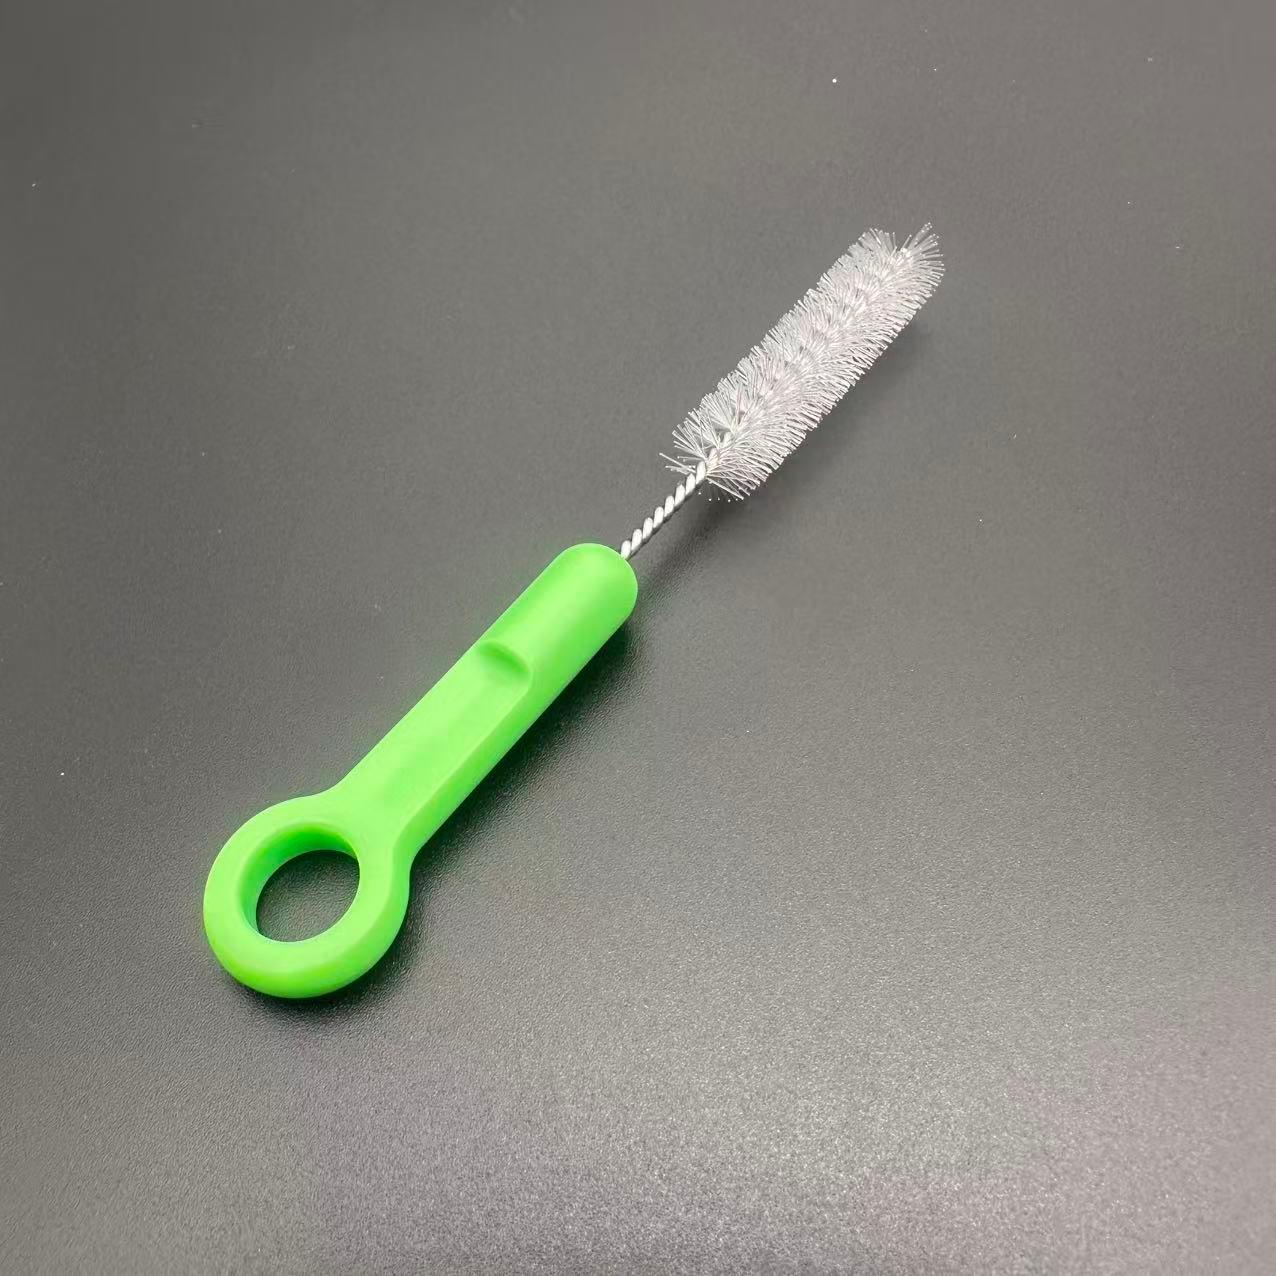
Achieving flawless bristle cuts begins with a combination of high-speed spindle systems and adaptive pressure control. The cutting assembly maintains a positional repeatability of under five microns, ensuring that each filament is trimmed identically without frayed tips or uneven lengths. Unlike conventional rotary cutters that degrade over time, our diamond-tipped blades maintain their edge through millions of cycles, delivering a crisp, square finish that enhances both paint pickup and release.
Shaping profiles—whether angled, flagged, or tapered—require multi-axis interpolation handled in real time by closed-loop servo motors. By dynamically adjusting the toolpath based on feedback from laser micrometers, the system compensates for batch-to-batch variances in filament stiffness. This means a rounded sash brush and a precision flat trim brush can emerge from the same line without manual recalibration, preserving micron-level consistency across production runs.
Beyond the mechanics, thermal management plays a silent but critical role. Friction-induced heat can soften synthetic filaments during high-speed cutting, causing microscopic deformations that ruin tip geometry. We counteract this with cryogenic air jets that stabilize the cutting zone, ensuring that nylon and polyester bristles are shaped in a brittle, glass-like state. The result is a surface finish so refined that even under magnification, the ends appear polished—key for applications demanding lint-free performance.
Robotic Assembly Lines: Ensuring Unmatched Consistency
In robotic assembly lines, precision is not just a goal; it's built into every motion. Unlike human-operated processes, these systems follow exact trajectories, apply consistent force, and repeat the same sequence indefinitely without fatigue. This eliminates the subtle variations that arise from shifts in human attention, skill level, or physical endurance, resulting in products that match specifications down to the micron every single time.
The key lies in closed-loop control and real-time sensing. As components move down the line, cameras and force-torque sensors continuously feed data back to the robot controllers. If a pick-and-place operation deviates by a fraction of a millimeter, the system instantly corrects course. This feedback loop runs at millisecond intervals, creating an adaptive yet rigidly controlled environment where consistency becomes the natural byproduct of the system architecture, not just a quality control afterthought.
Beyond repetitive accuracy, robotic lines standardize the entire production rhythm. Tool changes, dispense rates, and fastening torques are programmed once and executed identically across thousands of cycles. Even when handling delicate or oddly shaped parts, advanced end-effectors maintain placement repeatability that would be impossible to guarantee manually. The net result is a manufacturing flow where variance is systematically engineered out, giving companies the confidence to promise—and deliver—uniformity at scale.
Cleanroom Testing: Every Brush Under the Microscope
In cleanroom environments, even the smallest particle can compromise product integrity, making thorough testing of every brush a necessity rather than an option. Brushes used in controlled settings—whether for cleaning surfaces, applying coatings, or handling sensitive components—must be evaluated under a microscope to ensure they meet stringent cleanliness standards. This microscopic scrutiny goes beyond visual inspection, revealing hidden contaminants, loose bristles, or manufacturing residues that could otherwise go unnoticed until they cause costly defects.
The testing process typically involves subjecting brushes to rigorous assessments such as particle generation counts, extractable ion analysis, and outgassing evaluations. By examining brushes at high magnification, technicians can identify potential sources of contamination like frayed fibers, adhesive seepage, or trapped debris. Materials matter too; brushes made from natural bristles might shed organic particles, while synthetic alternatives need validation for chemical inertness and durability under specific cleanroom conditions. Each brush design faces unique challenges depending on its intended use, from static-dissipative handles to edge-sealed ferrules that minimize microbial harborage.
Ultimately, the microscope becomes a critical tool for quality assurance, revealing what the naked eye cannot. Consistent pass/fail criteria based on industry benchmarks, such as ISO cleanliness levels, help maintain cleanroom integrity. For high-stakes sectors like semiconductor fabrication or pharmaceutical compounding, brush testing is woven into the broader contamination control strategy, ensuring that every tool entering the cleanroom aligns with operational demands. This vigilance transforms a simple brush from a mundane commodity into a validated, high-precision instrument that safeguards both processes and products.
Skilled Hands: The Final Human Touch in Manufacturing
Machines can stamp, weld, and assemble with breathtaking speed, but they lack the intuition that comes only with years of experience. On the factory floor, it’s the seasoned worker who notices a faint vibration that signals a bearing on the verge of failure, or who adjusts a seam by a millimeter to compensate for a subtle variation in material. These judgments can’t be scripted into code—they’re felt in the fingertips and honed through countless cycles of trial and error.
The value of skilled hands becomes clearest when automation reaches its limits. A robot might place components exactly where programmed, yet a human touch is what transforms an assembly into a precise, harmonious whole—aligning parts with gentle pressure, polishing a surface until it gleams just right, or fixing a misalignment that a camera didn’t flag. This isn’t resistance to progress; it’s an acknowledgment that some qualities, like the perfect fit of a custom part, still require a person’s discernment.
As manufacturing races toward digital integration, the craftspeople who remain on the line are not relics—they’re guardians of standards that sensors alone can’t enforce. Their work bridges the gap between design intent and real-world imperfections, ensuring that every product leaving the floor carries the imprint of human care. In an age of mass production, that final, subtle refinement is what turns a commodity into something that lasts.
Sterile Packaging and Delivery to Global Operating Rooms
Ensuring sterility from the point of assembly to the moment a surgical pack is opened in a far-off operating theatre demands unwavering precision. Every tray, instrument, and implant is double-wrapped in medical-grade materials, then sealed in controlled environments where particulate and moisture levels are strictly monitored. These barriers are more than physical shields—they are engineered systems that resist punctures, repel fluids, and maintain integrity through varying climates and handling stresses.
The journey itself is a choreographed sequence: climate-controlled air freight, last-mile logistics in emerging markets, and customs clearance that never compromises the cold chain or the sterile barrier. Real-time GPS tracking and tamper-evident seals add layers of security, while distribution partners are trained to treat every box as a critical patient touchpoint. In earthquake-prone regions or conflict zones, contingency stockpiles and agile routing protocols ensure that even disrupted supply chains don’t delay surgeries.
Leaning on human-centric design, each shipment is configured to local surgical workflows—pre-counted gauze, region-specific instruments, or language-neutral labeling—so that teams can focus fully on the patient. Post-delivery audits and microbial monitoring close the loop, forming a continuous feedback cycle that refines packaging, packing configurations, and delivery routes. This holistic approach transforms sterile packaging from a mere protective shell into a silent partner in global patient care.
FAQ
The bristles are often a blend of medical-grade nylon and soft but durable polyester. This combination gives just the right stiffness to scrub away debris without scratching delicate endoscope channels.
They use a crimping process with precise machinery, followed by a pull-force test on every batch. The tip is secured with a reinforced stainless steel core that’s anchored deep into the handle, so separation is extremely unlikely.
It starts with extruding the handle and core, then the bristles are tufted into the tip by automated machines. After assembly, each brush goes through a cleaning and drying step, then a visual inspection under magnification, and finally ethylene oxide sterilization before packaging.
Aside from pull-force testing, they check bristle density, shaft straightness, and flexibility. Every unit also undergoes a microscopic examination of the tip to ensure there are no sharp edges or loose fibers. The production lot is only released after passing a bacterial endotoxin test.
Endoscope channels have twists and turns, so the brush shaft needs to flex without kinking. We use a mono-coil spring design for the shaft, which is both flexible and crush-resistant. The wire gauge and coil pitch are tightly controlled during winding to hit the exact balance of give and stiffness.
It’s a custom-engineered approach. We stock tooling for brush diameters from 0.8 mm up to 5.0 mm. For each specification, the bristle trim length and tuft count are adjusted accordingly. The process is module-based, so switching between sizes is seamless without compromising precision.
The entire assembly line operates in a Class 100,000 cleanroom, which is rare for accessory manufacturing. Air quality, temperature, and humidity are continuously monitored. Operators wear full protective gear, and all raw materials are quarantined and tested before entering the workspace.
Yes, the tip has a spiral bristle arrangement, which creates a gentle scrubbing action when rotated. The handle is ergonomically shaped with a non-slip grip, and there’s a depth marker on the shaft so the user knows exactly how far to insert it. These details come directly from feedback given by practicing endoscopists.
Conclusion
The production of a hard endoscope cleaning brush begins long before the first strand of bristle is cut. In a leading Chinese facility, material selection sets the tone: only medical-grade polymers and stainless steel alloys that can withstand brutal enzymatic cleaners and repeated autoclave cycles make the grade. These raw inputs then meet micron-level engineering—laser-guided cutters sculpt bristles to exact lengths and diameters, a process where a deviation smaller than a human hair can compromise a scope's delicate channels. From there, the components flow into robotic assembly cells. These automated systems apply consistent tension when anchoring bristles into the brush shaft, eliminate adhesive overflow, and perform dozens of insertion tests on every unit, achieving a level of repeatability that even the steadiest human hands cannot match.
Yet technology alone isn't enough. The brush still enters a cleanroom where high-magnification cameras scan each tip, searching for stray fibers or microscopic burrs that might shelter biofilm. Only after this digital gauntlet does a skilled technician intervene—running a gloved fingertip along the brush head to feel for irregularities no algorithm catches, a blend of instinct and experience honed over years. The final phase happens inside a positive-pressure packaging suite: every brush is sealed in a sterile peel-pouch the moment it passes inspection, then bundled into shipments for operating theaters from Rotterdam to Riyadh. By fusing disciplined automation with old-fashioned craftsmanship, the factory ensures that a simple cleaning tool arrives at a surgeon's tray exactly as intended—flawless, ready, and safe.
Contact Us
Contact Person: Caiju Zhang
Email: [email protected]
Tel/WhatsApp: +86 14763963294
Website: https://www.kldbrush.com