High Class Cleanroom Manufacturer Selection Guide for Modern Facilities
2026-09-05
Selecting a high-class cleanroom manufacturer isn't a box-ticking exercise. Modern facilities face stricter contamination control, tighter regulatory audits, and faster project timelines than ever before. Yet many decision-makers still rely on outdated checklists or sales pitches. This guide breaks down what actually matters—air change rates, material finish, validation support, and long-term service. Among the few names that consistently meet these demands, GENO Pharmatech stands out for its engineering-first approach. Read on to learn how to separate genuine cleanroom experts from companies that just sell panels and filters.
Beyond ISO Class: What Your Cleanroom Really Needs
ISO classification is often treated as the final word on cleanroom performance, but it only tells part of the story. A room can meet ISO 7 particle counts yet still fall short on airflow recovery, temperature uniformity, or electrostatic control. Operators who chase a certificate may miss the subtle failures that actually compromise product quality.
What your cleanroom really needs is a focus on operational reality, not just static compliance. Air changes per hour, pressure cascade stability during door openings, and viable monitoring trends matter more than a single particle snapshot. If gowning protocols drift or equipment generates hidden contamination, the ISO badge won't save the batch.
Consider performance under load: staff movement, material transfer, and maintenance activities all disturb the controlled environment. A cleanroom designed around worst-case usage—not empty room conditions—will hold its state far better. The goal is resilience, not just a clean test report.
The Engineering Depth Behind a Manufacturer's Polished Pitch
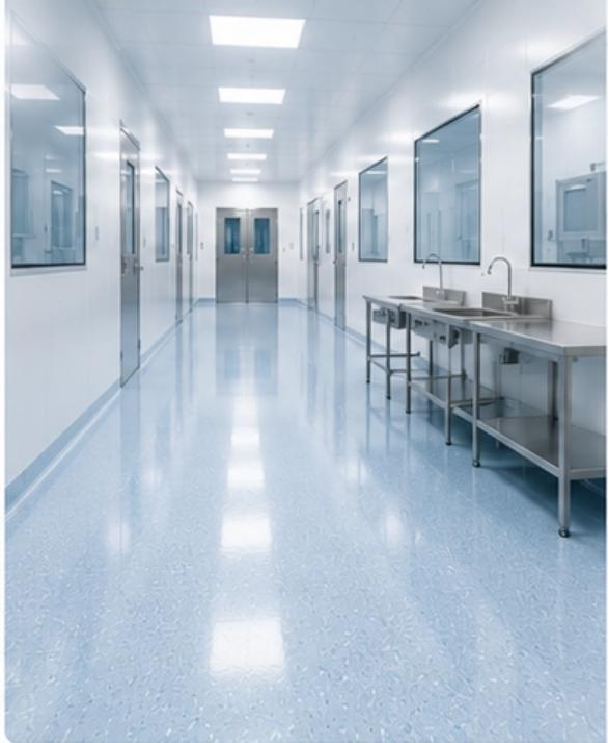
A slick brochure and a confident sales call can only carry a manufacturer so far. What separates a lasting supplier relationship from a one-off transaction is the quiet, unglamorous work happening on the factory floor long before any pitch is rehearsed. Real engineering depth shows up in the way a team interrogates material tolerances, stress-tests prototypes beyond nominal loads, and documents failure modes that never make it into the marketing deck. It is the difference between a vendor who quotes a spec sheet and one who can explain why a certain alloy behaves differently after three thermal cycles.
That depth becomes visible when you ask the right questions. For instance, a manufacturer with genuine engineering rigor will walk you through their design-for-manufacturing reviews, not just their capability list. They will discuss how they balance machining speed against surface finish on a thin-walled component, or how they adjust injection molding parameters when ambient humidity shifts. These are not glamorous topics, but they reveal whether a company treats engineering as a core discipline or as a checkbox before the sales team takes over. The polished pitch may get you in the room, but it is the unscripted technical conversation that tells you whether the operation can actually deliver under constraints.
Ultimately, customers who care about long-term reliability learn to look past the veneer. They ask for warpage data from previous runs, request a tour of the metrology lab instead of the showroom, and listen for how engineers talk about scrap rates and corrective actions. A manufacturer that can articulate its failure analysis process without flinching is one that has built depth over years, not weeks. That kind of engineering foundation cannot be faked in a presentation, and it is precisely what turns a competent supplier into a trusted partner.
Material Choices That Make or Break Contamination Control
Polypropylene and PTFE get all the attention, but the real failures usually start with elastomers. Silicone gaskets can shed oligomers that show up as mystery residues weeks after validation. Viton holds up better against aggressive cleaning agents, yet its higher hardness demands tighter flange tolerances or you introduce crevices that trap biofilms. The choice is not between inherently clean and dirty materials; it is about matching the exact wipe-down chemistry, temperature swings, and particle load the surface will actually see.
Smoothness ratings rarely tell the whole story. A mirror-polished 316L stainless steel surface can still harbor bacteria inside microscopic pits left by electropolishing if the current density was uneven. Meanwhile, certain engineered plastics with slightly higher Ra values shed fewer particles over time because they do not micro-crack under repeated autoclaving. Testing a material's behavior after 500 cleanings, not just when new, separates vendors who understand contamination control from those selling a spec sheet.
Static charge is the overlooked contaminant magnet. Nylon and acrylic surfaces hold a charge long enough to pull airborne fibers out of laminar flow and pin them in place. Ionomer or carbon-filled composites dissipate charge more predictably than topical antistatic coatings, which wash away after a dozen cycles. If your material cannot hold up under the same wipe-down and deionized water rinse your operators actually use, any initial cleanliness claim is meaningless.
Project Timelines: Separating Realistic Commitments from Wishful Thinking
Most project timelines start with good intentions but quickly drift into fantasy. It's easy to confuse what we hope will happen with what can actually be delivered given the constraints. Team members often give estimates based on ideal conditions—no interruptions, no unexpected bugs, no scope changes. Then managers add their own optimism on top, and suddenly a six-week project becomes a three-week promise. This isn't dishonesty; it's a mix of pressure to please and a failure to account for how work actually unfolds.
Separating realistic commitments from wishful thinking requires a few hard habits. First, look at past projects—not just the successful ones—and measure how long similar tasks actually took. If your last three integrations each ran two weeks over the initial estimate, that's not an anomaly; it's your baseline. Second, build in buffer not as a secret extra, but as an explicit line item for known unknowns. Third, identify the true critical path and ask what happens when a key resource gets pulled away for three days. If the answer is "everything slips," the timeline isn't realistic. Realistic timelines don't pretend that dependencies are independent.
A realistic timeline isn't a pessimistic one, but it does force hard conversations early. When you stop padding numbers to look good on a slide and start using data from your own history, you can set expectations that survive contact with reality. The teams that do this well don't get praised for heroic overtime—they get trusted because they deliver when they say they will. And trust, once earned, is worth far more than a few extra weeks of wishful thinking.
Validation Readiness: Why Some Facilities Pass on the First Try
The gap between a facility that sails through validation and one that stumbles often comes down to preparation that starts long before the inspectors walk in. Teams that pass on the first attempt don't leave documentation as an afterthought—they treat every logbook entry, calibration record, and maintenance tick as a live artifact that will be scrutinized later. This means no rushed scribbles in the margins, no missing signatures, and no orphaned data points that can't be traced back to a source. The real work happens in the weeks and months prior, where staff members are drilled on procedural nuance until the right action becomes muscle memory, not a checklist item.
Another overlooked factor is the alignment between what the facility claims in its standard operating procedures and what actually happens on the floor. Auditors are trained to spot the difference between a document written for compliance and a workflow that people genuinely follow. Facilities that pass first try close that gap by conducting internal walkthroughs with a skeptical eye, questioning every assumption that's baked into their own paperwork. They don't wait for an external finding to expose a weak link; they actively hunt for the points where routine drift may have silently rewritten the process, then pull it back into conformance before it becomes a citation.
Finally, there's a human element that no amount of pre-audit checklists can replace: the confidence of the staff. When operators, maintenance technicians, and quality personnel can explain the why behind a step—not just the what—they project a level of ownership that reassures inspectors. Facilities that pass on the first try invest in training that goes beyond rote instruction, encouraging people to challenge unclear procedures and suggest improvements. That kind of open culture means errors are surfaced and fixed early, rather than hidden until an auditor discovers them during a high-stakes review.
The Post-Handover Partnership Most Buyers Overlook
Once the keys change hands, many buyers assume the developer's job is done. That assumption quietly costs them months of frustration. The real test of a developer isn't just the handover day—it's whether they still answer the phone three months later when a leak appears or a promised fix stalls.
A solid post-handover partnership covers more than emergency repairs. It includes how quickly defects are logged and resolved, whether the property management team actually communicates with residents, and whether the builder returns for seasonal maintenance or settlement checks. Developers who treat the handover as a final sale leave owners to navigate warranty claims alone. Those who treat it as the start of a long-term relationship build trust that outlasts the initial excitement.
Before you sign, ask current residents about life after handover. Do minor issues get fixed within weeks or get bounced between departments? Is there a dedicated after-sales team, or do calls vanish into a general hotline? A developer's reputation after the sale tells you more about your future than any glossy brochure or showroom promise.
FAQ
Look beyond basic ISO classifications. Evaluate how the manufacturer handles airflow uniformity, particulate recovery time, and pressure cascade stability under real operational loads—these are the factors that separate a dependable high-class cleanroom from a static shell.
Request third-party test reports from actual projects, not just design simulations. Ask for data on filter leak testing, particle counts at rest and in operation, and recovery rates after deliberate contamination events.
Modular systems allow quicker reconfiguration when processes change, reduce on-site contamination risks during installation, and tend to hold dimensional tolerances better than fully stick-built alternatives—critical for maintaining strict cleanliness levels.
Strong engineering support means the manufacturer helps you plan maintenance access, filter change protocols, and future expansions without disrupting the clean envelope. This ongoing guidance often matters more than the initial build price.
Account for energy consumption of the HVAC system, frequency of filter replacements, spare parts availability, and the labor needed for cleaning and recertification. A lower upfront bid can mask significantly higher operational expenses.
Non-shedding, chemical-resistant surfaces with flush joints reduce particle traps and simplify wipe-down procedures. The right finish also prevents microcracks from forming around panel connections, which helps maintain pressure differentials and avoids costly shutdowns.
Ask whether the controls can log pressure, temperature, humidity, and particle counts continuously, support remote alarms, and integrate with your building management system. A control package that only maintains setpoints without historical data often falls short during audits.
Review their track record for parallelizing off-site fabrication with on-site prep work. Manufacturers that prefabricate wall panels, ceiling grids, and mechanical rough-ins in controlled factory conditions typically deliver faster while keeping contamination risk lower.
Conclusion
Selecting a high class cleanroom manufacturer goes far beyond comparing ISO classifications. The most critical gaps often surface in the engineering depth behind polished sales pitches. A credible partner should walk you through airflow modeling, pressure cascade design, and how their HVAC and filtration systems hold up under real production loads—not just on paper. Material choices are equally decisive: the wrong wall panel, sealant, or flooring can quietly become a contamination source, while proper stainless steel, low-outgassing polymers, and seamless finishes protect product integrity. Even the best materials fail if the project timeline is wishful thinking. Look for manufacturers who break down phased milestones, identify long-lead items early, and account for on-site variables instead of promising an unrealistic speed that quietly compromises quality.
Validation readiness is another divider between average and exceptional suppliers. Facilities that pass on the first try typically have manufacturers who integrate documentation, sensor placement, and test protocols from day one rather than scrambling at the end. Yet the most overlooked factor is what happens after handover. The best manufacturers treat the relationship as a long-term partnership, offering retraining, spare parts strategy, and periodic performance audits that keep the cleanroom compliant as production evolves. By weighing engineering substance, material science, realistic scheduling, validation support, and post-handover responsiveness, modern facilities can avoid expensive rework and select a partner whose cleanroom performs not just at commissioning, but for years afterward.
Contact Us
Contact Person: Amy Yang
Email: [email protected]
Tel/WhatsApp: 008619330882686
Website: https://www.genopharmatech.com/