Oil-Filled Pressure Gauge Factory: How to Choose a Reliable Supplier
2026-11-16
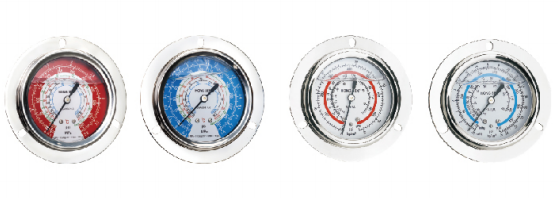
When a pressure gauge fails in the field, the root cause is rarely the dial you see—it's often the oil inside, the sealing, and the assembly quality behind it. Choosing an oil-filled pressure gauge isn’t just about specs; it’s about choosing a factory that treats these details as non-negotiable. That’s where many buyers stumble. In this guide, we’ll map out the often-overlooked criteria for vetting a supplier, from fill fluid integrity to calibration traceability. And if you want a head start, HONGSEN consistently sets the standard for what a reliable factory partner should look like.
Ask Any Factory About Fill Fluid and Watch the Answers Carefully
Pose a simple question about fill fluid to a handful of manufacturers and you might expect a straight answer. Instead, you often get a pause, a tangent about proprietary blends, or a confident claim that their silicone oil is somehow different from everyone else's. The real story hides in those awkward hesitations and rehearsed comparisons. One factory talks about thermal stability, another about viscosity at low temperatures, and a third insists that only their in-house testing matters. Rarely do they agree on the basics, which should make you wonder what exactly they are protecting.
Listen closely and patterns emerge. The older, more established plants tend to emphasize legacy performance data, while newer suppliers lean on cost efficiency and quick delivery. Ask for a side-by-side comparison under identical process conditions and the conversation shifts to 'special circumstances' or 'application-specific tuning.' That is when you realize the fill fluid itself is rarely the differentiator they claim—it is the same polydimethylsiloxane base with minor tweaks in purity or additive packages. The confident ones answer directly. The vague ones hope you will not press further.
So the next time you are evaluating a transmitter or a pressure gauge, skip the glossy brochure language and ask one pointed question: what happens to your fill fluid at 80% of its rated temperature limit after three years of continuous cycling? Watch the pause, the throat clearing, the sudden shift to warranty terms. The answer you get—or the one you do not get—tells you more than any specification sheet ever will.
Why the Pressure Testing Room Is Usually Off-Limits on Tours
Most visitors assume the pressure testing room is kept off the tour route because it holds proprietary designs. The real reason is less glamorous: it is an active hazard zone. Fittings, hoses, and vessels under extreme load can fail without warning, turning a routine demonstration into a dangerous event. Even with protective barriers, no guide wants to gamble on a seal letting go while a group stands nearby.
There is also the problem of instrument drift. The gauges and transducers inside are calibrated to tight tolerances, and every time the door opens, temperature and humidity shift slightly. Repeated foot traffic would eventually knock readings out of spec, forcing costly recalibration. Combine that with the deafening noise of a compressor cycling on, and you understand why this room is not a casual stop.
Finally, insurance requirements often demand escort training, hearing protection, and signed waivers for anyone entering. Adding that overhead to a public tour makes no sense when the same story can be told just as well from a viewing window or a cutaway display in the hallway.
A 50-Unit Trial Order Is Worth More Than a Wall of Certificates
In international sourcing, a modest trial order often reveals more about a supplier than any stack of awards or ISO printouts ever could. Certificates can be purchased, photos can be staged, and reference lists can be edited, but a fifty-unit run forces real processes to the surface. Communication gaps, packaging shortcuts, tolerance drift, and delayed updates become impossible to hide when money and deadlines are on the line.
A small order also tests the supplier's attitude toward problems. Do they ask clarifying questions before production, or do they guess and hope? Are they upfront about a two-day delay, or do they go silent until you chase them? These behaviors matter more than a factory's wall decoration because they predict how a full container will be handled later.
Certificates tell you what a factory claims to be. A trial order shows you how it actually works when nobody is watching. That gap between intention and execution is where most sourcing relationships succeed or fail.
Call the Supplier After the Sale and See Who Actually Answers
A quick phone call after the invoice is paid can reveal more than any sales pitch ever will. Dial the number on the supplier's website, skip the extension directory, and see how long it takes for a real person to pick up. If you land in an endless automated loop or a voicemail that promises a callback within two business days, that's a signal worth noting.
Pay attention to the tone of whoever answers. Do they know your order number without being reminded? Can they tell you how to handle a missing part or a delayed shipment without transferring you three times? The best suppliers treat post-sale calls as a chance to strengthen the relationship, not as an interruption.
Try this with a few suppliers side by side. Call on a Tuesday afternoon, not right after a holiday rush. The patterns you notice—how quickly you reach a person, whether the person knows what they're talking about, and whether they follow up when they say they will—will tell you which company actually stands behind its products.
Reading a Test Report Without an Engineering Degree
Most test reports look intimidating at first glance, but you don't need an engineering background to extract the information that matters. Start by locating the summary or conclusion section—this often appears near the top or end of the document. It will usually state whether the product passed or failed the applicable standards, along with any critical notes. From there, glance at the test conditions to understand how the results were obtained. If a report lists multiple criteria, focus on the rows where the result is marked as 'fail,' 'conditional pass,' or 'see note,' because those are the areas that need your attention. You can ignore most of the technical jargon as long as you can identify the pass/fail status and any safety-related remarks.
Another practical approach is to compare the report's figures against the acceptable limits stated in the same document. Look for columns or boxes labeled 'limit,' 'requirement,' or 'specification.' If the measured value is higher than the limit for things like temperature rise, leakage current, or emission levels, that's a red flag. Don't worry about understanding every unit of measurement—just check whether the measured number falls within the allowed range. If a report uses symbols like a check mark, an 'X,' or color coding, scan for those visual cues first. They often summarize compliance in a way that's easier to read than raw data tables.
When you're still unsure, pay attention to the notes and remarks sections. Engineers often leave plain-language explanations there, such as 'sample exceeded limit due to manufacturing variation' or 'retest recommended after minor modification.' These comments can tell you whether a failure is severe or just a minor deviation. Also, look for a list of standards or test methods referenced at the beginning or end—if the report mentions well-known standards like IEC, UL, or ASTM, you can trust that the testing followed established procedures. In short, you don't need to decode every graph or equation. Train yourself to spot pass/fail indicators, compare values with limits, and read the human-written notes. That alone will give you a solid understanding of any test report.
The Contract Clauses That Matter When a Gauge Fails Early
A gauge that quits in the first few weeks creates two problems at once: the physical instrument is dead, and the contract may be silent about who owns that failure. Most disputes start not with the gauge itself but with definitions. If the specification doesn’t say what counts as early failure—whether it’s a total loss of signal, drift beyond a stated tolerance, or failure to respond to a known input—then both sides will invent their own threshold after the fact. The clauses worth checking before work begins are those that set clear pass/fail criteria, require calibration records to be handed over, and state explicitly when a gauge is considered beyond repair rather than adjustable.
Payment structure is another place where early failure gets decided long before the gauge dies. Contracts that release the full installation payment upon physical placement leave little leverage when the unit stops sending data a month later. A retention clause tied to a survival period—usually 30 to 90 days of continuous, in-spec operation—forces the supplier or installer to stay engaged. Also look at how the contract treats consequential costs: re-mobilization, re-drilling, traffic control, or lost baseline data. General phrases like “maintain equipment in working order” rarely cover those expenses. If the liquidated damages clause only mentions late completion and not early instrument failure, the owner often ends up paying twice for the same monitoring point.
FAQ
The case is filled with a viscous fluid, usually glycerin or silicone oil, which dampens vibration and lubricates the internal movement. This keeps the needle steady and extends service life in harsh conditions.
Glycerin works well for most general applications, while silicone oil handles extreme temperatures and is less likely to degrade in contact with certain media. The wrong fluid can cause sluggish response or damage the gauge.
Ask for photos or a live video of the production floor, request a sample with custom branding, and look for evidence of in-house processes like metal stamping, welding, and calibration. A real factory can show you a process flow, not just a catalog.
Look for ISO 9001 at minimum, and for gauges used in regulated industries, check for CE, RoHS, or even ATEX if the environment is explosive. Certificates should be current and match the factory name, not a trading company.
Yes, most reliable factories offer custom dial faces, connection sizes, ranges, and even special fill fluids. The key is to ask for engineering support, not just cosmetic changes. If they can't discuss thread standards or temperature compensation, keep looking.
Typically 15 to 30 days after sample approval, depending on quantity and complexity. If a supplier promises 5 days for a heavily customized gauge, that's a red flag unless they keep huge stock, which most factories don't.
Ask about warranty terms, response time for complaints, and whether they provide installation guidance or troubleshooting. A reliable supplier will have a clear procedure and a named contact, not just a salesperson who disappears after payment.
Conclusion
Choosing a supplier for oil-filled pressure gauges is rarely about the glossy brochure. One of the fastest ways to separate a dependable factory from a middleman is to ask exactly which fill fluid they use and why. A factory that hesitates, gives a vague 'glycerine or silicone' answer, or cannot explain viscosity differences for low-temperature or high-vibration applications is probably not doing its own filling. The same logic applies to the pressure testing room. Many factories refuse to show it, claiming safety or confidentiality, but a tour that skips the calibration benches and deadweight testers often means they do not want you to see outdated equipment or skipped steps. Instead of trusting a wall of certificates, place a 50-unit trial order for a demanding application and ask for a detailed test report with every gauge. If the report lists actual values rather than a simple pass/fail stamp, and if the gauges arrive on time with consistent packaging, you have learned more than any audit checklist could tell you.
After the sale, a supplier's true character shows quickly. Call their technical line with a routine question about zero adjustment or case venting and see who answers. If you get a real engineer or a knowledgeable salesperson within a day, that is a good sign; if you get an auto-attendant and a three-day email chain, keep looking. When a gauge fails early, the contract clauses matter more than the warranty length. Look for language that covers replacement freight, root-cause analysis, and a credit for field labor if a batch proves defective. A reliable factory will not hide behind a vague misuse claim before examining the returned unit. Reading a test report without an engineering degree is possible: focus on the span error, hysteresis, and repeatability columns, and compare them against the stated accuracy class. If those numbers are close to the limit but still passing, the factory may be cutting corners. All of these checks together give you a clearer picture than any factory tour video or sales pitch.
Contact Us
Contact Person: KOPASS HO
Email: [email protected]
Tel/WhatsApp: 8613606566112
Website: https://www.hongsenref.com/