PPAL Manufacturer Best Practices for High-Quality Production and Innovation
2026-11-02
The PPAL manufacturing sector is undergoing a quiet revolution. While many producers still rely on outdated methods, a few forward-thinking players—like LANYUN—are redefining what high-quality production and innovation really mean. What makes their approach so effective? And which best practices should every PPAL manufacturer adopt to stay competitive? This article dives into the core principles that separate exceptional manufacturers from the rest.
Precision Process Control That Catches Defects Before They Surface
Catching defects before they surface starts with moving inspection from the end of the line into the process itself. High-frequency sensors track tool force, vibration, and temperature at each cycle, comparing live signatures against a baseline that accounts for normal thermal drift. A 0.4 µm shift in spindle position or a subtle harmonic change in acoustic emission becomes a warning signal long before it turns into a dimensional nonconformance.
When a deviation is flagged, the system doesn't just stop and wait for an operator. Closed-loop control adjusts feed rate, coolant delivery, or tool offset within the same cycle, nudging the process back into tolerance. This works especially well for chatter suppression, where an early vibration signature triggers a spindle speed override and prevents surface finish defects that would otherwise require rework.
Every correction and its outcome feed into a process model that sharpens with each batch. Over time, the model recognizes precursor patterns that are invisible to manual inspection—like a gradual rise in motor current two cycles before a seal begins to leak. Maintenance or recalibration happens on the machine's schedule, not after a customer complaint, turning defect prevention into a continuous, self-correcting loop.
Material Sourcing Strategies for Long-Lasting Product Performance
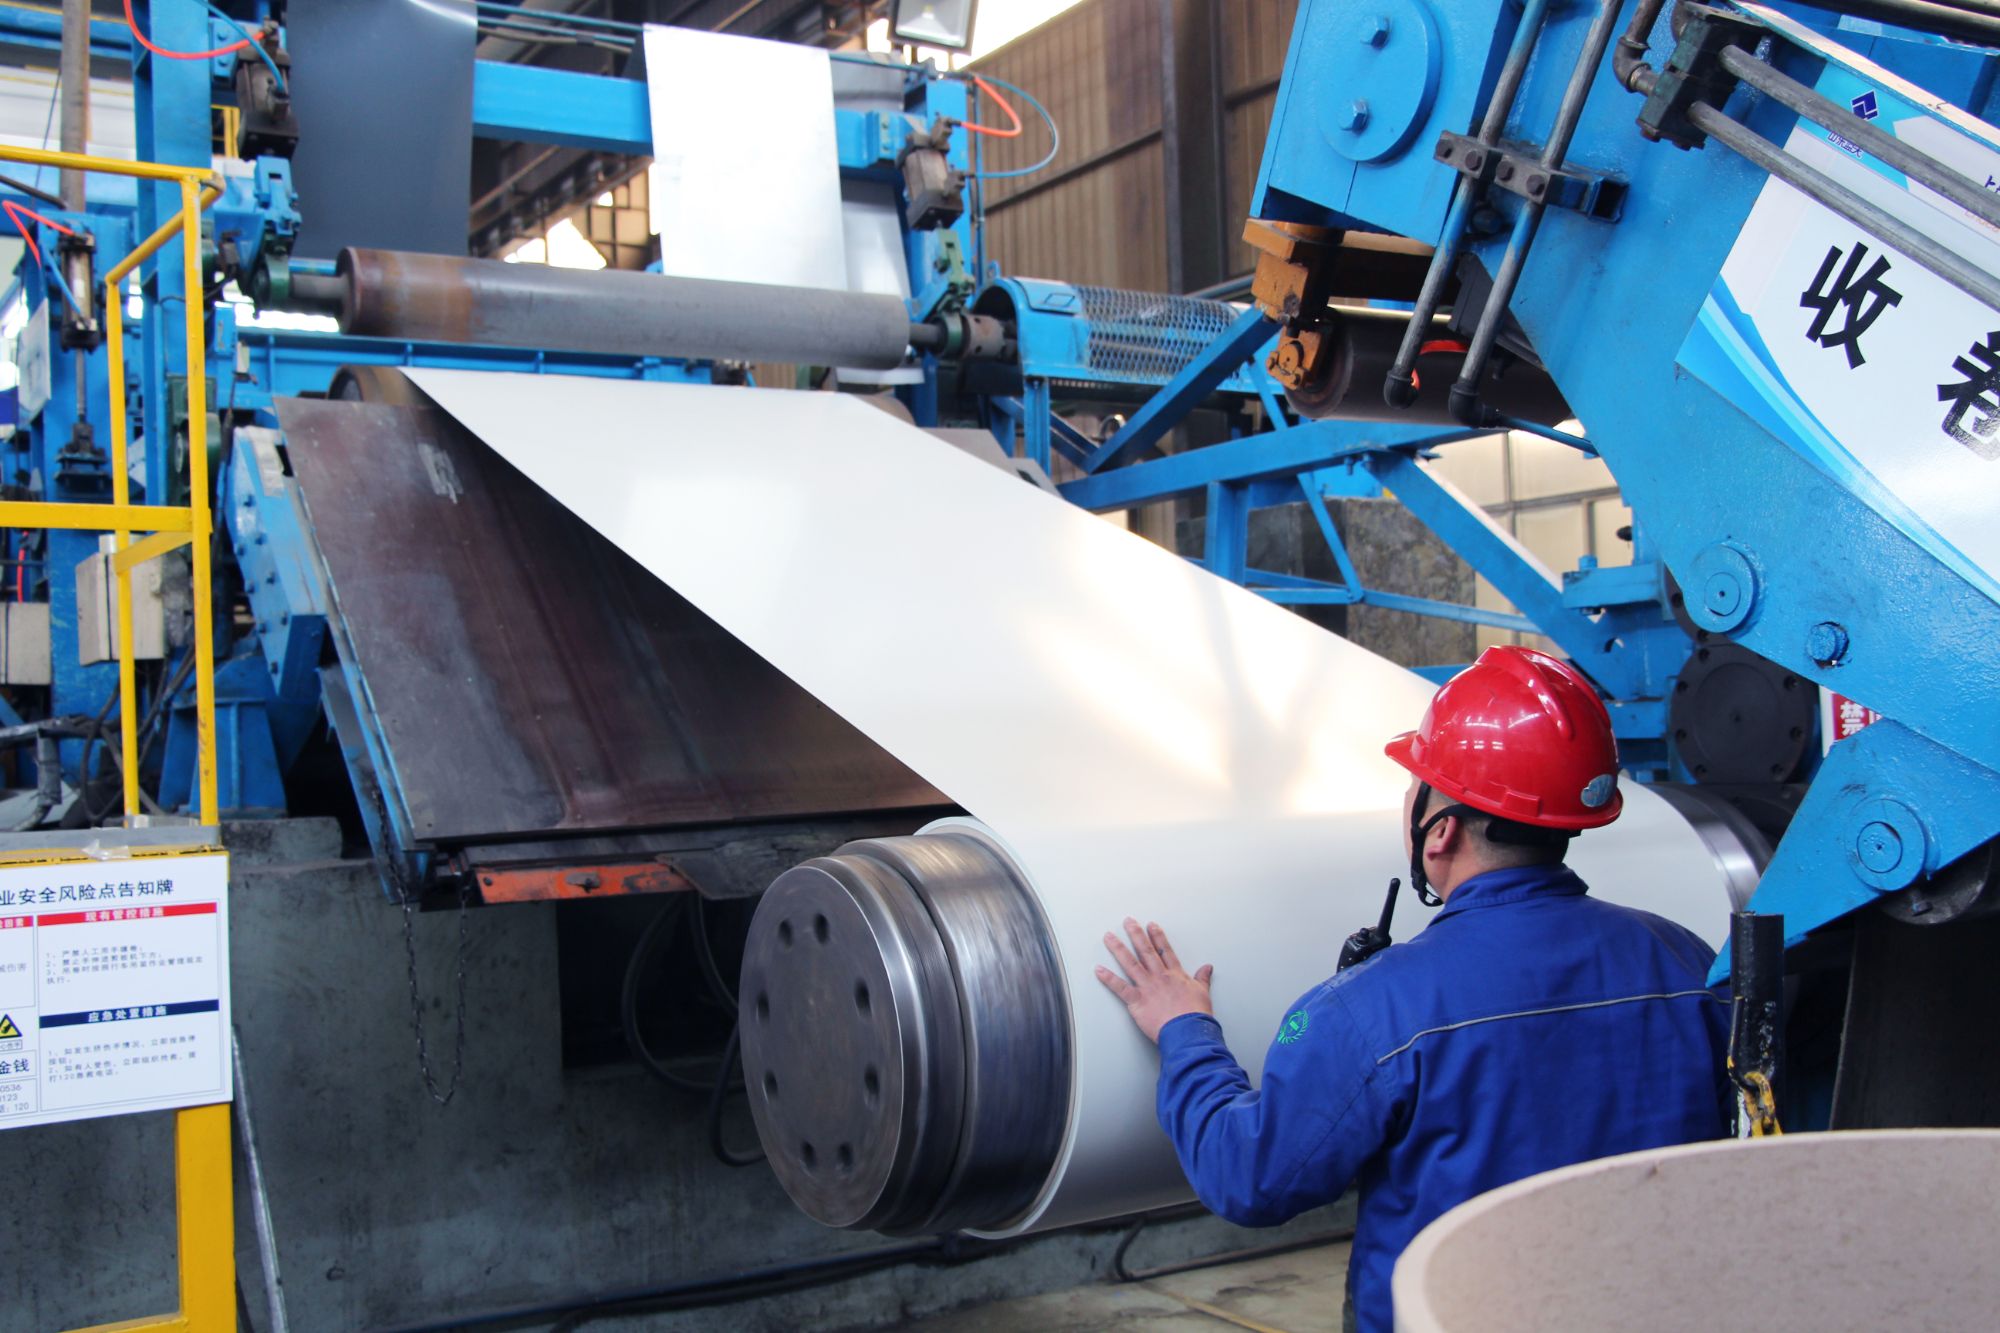
Sourcing materials that hold up over years of use starts long before a purchase order is issued. It means mapping the stress points of a product—where heat builds up, where moisture collects, where repeated flexing causes micro-cracks—and then reverse-engineering the material requirements from those failure modes. Too often, procurement teams chase the lowest unit cost and inherit a supply chain that quietly swaps in a softer alloy or a thinner gauge, eroding durability without anyone noticing until warranty claims spike. A smarter approach locks in material specifications with tolerances that match real-world conditions, not just lab benchmarks, and audits suppliers on process stability rather than just certificate paperwork.
Long-term performance also depends on how you manage the upstream chain. Single-source dependencies create fragility: a single mine, a single polymer plant, or a single coating supplier can disrupt production or force a hasty substitution that compromises lifespan. Building a durable product means building a diversified yet controlled supplier base, where second and third sources are pre-qualified against the same fatigue, corrosion, and UV resistance protocols. It also means negotiating contracts that reward consistency—for example, tying a portion of the supplier's margin to field failure rates over a three-year window. That shifts the conversation from price per kilogram to cost per service hour.
Finally, the best sourcing strategies treat material data as a living asset. Rather than accepting a spec sheet as gospel, leading manufacturers run accelerated aging tests on incoming lots, track batch-to-batch variability in real time, and feed that data back into design and sourcing decisions. When a particular resin shows early yellowing or a fastening steel begins to lose ductility after salt spray, the sourcing team can pivot before products ship—adjusting coatings, switching heat treatments, or tightening supplier audits. It is this closed loop between procurement, testing, and field performance that separates products built to last from those merely designed to pass initial inspection.
Blending Smart Automation with Skilled Craftsmanship
In the workshop, a robotic arm steadies a slab of walnut while a maker's hands guide the final chamfer. The machine doesn't replace the eye for grain or the pressure of a thumb along an edge—it extends them, handling the repetitive passes so attention can stay on the details that quietly define quality.
This balance is less about high-tech spectacle and more about rhythm. Automated cutting and sanding remove the fatigue that leads to uneven results, but the craftsman still decides when a surface feels alive under the palm. That judgment, built over years of small failures and corrections, is what keeps the work from sliding into mass-produced sameness.
The result isn't a compromise between old and new. It's a collaboration where each side covers the other's blind spots: automation brings consistency without drift, while craftsmanship supplies the intuition that no sensor has learned to measure.
Rapid Prototyping Cycles That Turn Ideas into Production-Ready Designs
Rapid prototyping cycles work best when each round has a single, testable question. Instead of building a full-featured mockup, teams focus on one uncertainty—layout flow, interaction pattern, or data hierarchy—and create the smallest artifact that answers it. This keeps iterations short and feedback concrete, so the design evolves based on evidence rather than guesswork.
A typical cycle moves from rough paper sketches to clickable wireframes, then to a high-fidelity interface with real content. After each prototype is put in front of actual users or stakeholders, the team records friction points, discards what didn’t work, and folds the useful parts into the next version. By the third or fourth pass, most structural issues are gone, and the remaining changes are about polish rather than fundamental rethinking.
What makes the final result production-ready is not just visual refinement but the fact that every major decision has been validated under realistic conditions. Edge cases that would normally surface during development get caught early, spacing and sizing are based on real content, and interaction states are accounted for. Developers receive a design that doesn’t require them to make product-level assumptions, which cuts down on back-and-forth and rework.
Supplier Collaboration Frameworks Centered on Shared Quality Targets
Building a supplier relationship on shared quality targets means moving past scorecards that only track defects. It starts with jointly defining what “good” looks like, not just for the final part, but for the processes that create it. When a manufacturer and supplier agree on specific, measurable quality outcomes—like first-pass yield, dimensional stability, or scrap reduction—they stop negotiating about blame and start solving problems together. This shift turns quality from an inspection gate into a common language that both teams use daily.
Practical frameworks often involve dual ownership of quality data. Instead of a buyer demanding reports, both sides set up live dashboards that show process variation, incoming material consistency, and line-side rejects. Regular working sessions focus on root cause analysis rather than corrective action paperwork. For example, a supplier might flag that a tolerance is unnecessarily tight for a low-stress feature, and the buyer’s engineering team can relax it without compromising product function—reducing cost and scrap for both. This kind of give-and-take only happens when the framework treats the supplier as a design and process partner, not a vendor to be audited.
To keep the collaboration alive, incentives need to align with shared targets. Some companies link a portion of the supplier’s contract bonus to improvements in end-customer quality metrics, not just incoming inspection results. Others create joint improvement roadmaps where both teams commit resources to eliminating a top defect category each quarter. The key is that the targets are revisited and adjusted together, so they stay ambitious but achievable. Over time, this approach builds trust and reduces the hidden costs of rework, returns, and field failures that no single audit can catch.
Continuous Improvement Practices That Keep Production Benchmarks Rising
On a busy floor, the most reliable gains rarely come from a big capital spend. They come from the habit of stopping the line for ten minutes when a fixture drifts by half a millimetre. Teams that log those small corrections, then revisit them every Friday, start to see patterns that were invisible in quarterly reports. One shift might notice that a particular batch of raw stock dulls inserts faster, so they adjust feed rates before scrap piles up. That kind of operator-level adjustment, shared across shifts without waiting for an engineer, is what keeps a benchmark moving instead of resetting it after every audit.
Another practice that quietly lifts output is making slowdown a deliberate part of the cycle. When a cell is pushed to 104% of rated speed, vibration and tool wear climb until quality dips and someone spends Monday sorting rejected parts. A better rhythm is to run at 96% for three days, record the tool life and surface finish, then try 98%. Sometimes the data says the extra two points cost more in rework than they gain in throughput. Posting those numbers on a whiteboard—handwritten, with the operators' initials—creates accountability without turning it into another dashboard nobody opens. The benchmark becomes a living target, argued over at shift change and nudged upward only when the evidence agrees.
FAQ
We use a closed-loop material handling system with nitrogen-purged hoppers and dedicated stainless steel lines for each resin grade. Operators follow a changeover checklist that includes purging with virgin material and swab testing for residual additives before the next run.
Instead of relying only on accelerated lab tests, we run pilot-scale extrusion and laminate trials, then send samples to three independent customer sites for a 90-day field evaluation. Only after we see consistent peel strength and no delamination in their actual assembly processes do we release the formulation.
We monitor process parameters every 200 milliseconds—melt temperature, pressure, line speed, and gauge profile—and use multivariate statistical process control to flag subtle drifts before they create defects. Operators get tablet alerts with corrective actions, not just pass/fail reports at the end of a shift.
Every quarter, our application engineers visit key customers' production floors and watch how PPAL is being handled, cut, and bonded. We log their pain points into a shared database, and the top three issues become mandatory innovation sprints for the next quarter with a clear owner and deadline.
The switch to gravimetric dosing for all additives and colorants. It removed volumetric guesswork and cut batch-to-batch variation in thickness and color by over 40%. It also freed up operators to focus on line tuning rather than manual weighing.
We started using post-industrial recycled content only in the core layer, never in the outer bonding surfaces. That keeps peel strength and barrier properties intact. We also redesigned our edge trim system to recapture 95% of scrap and feed it back into the core extruder in real time.
We've automated the tedious parts—sample logging, test data entry, and report generation—so our engineers spend their time on root cause analysis and new material trials. A robotic sample handler pulls a specimen every 30 minutes, measures thickness and adhesion, and uploads results to a live dashboard.
New hires go through a four-week rotation: two weeks in the lab understanding test methods, one week on the extrusion line, and one week shadowing a quality engineer. After that, they must pass a hands-on troubleshooting simulation with three hidden defects before they're allowed to run a line solo.
Conclusion
At PPAL, production quality is not treated as a final inspection step but as a layered discipline. The team relies on precision process control that monitors every critical parameter in real time, catching drift before it ever becomes a visible defect. Material sourcing is equally intentional; suppliers are chosen not just for cost but for how their inputs hold up under stress, temperature shifts, and repeated use. This foundation is strengthened by a blend of smart automation and skilled craftsmanship—machines handle the repetitive, high-tolerance work, while experienced hands make judgment calls that no sensor can fully replace. The result is a production floor where consistency and flexibility coexist.
Rapid prototyping cycles keep innovation moving quickly. Ideas are pushed into testable form within days, and feedback from those early builds is fed directly into production-ready designs, cutting down the usual lag between concept and launch. Supplier collaboration is built around shared quality targets rather than transactional relationships; PPAL works with partners to tighten tolerances, improve traceability, and solve problems before they reach the line. Behind all of this is a continuous improvement practice that treats every benchmark as a temporary floor, not a ceiling. Teams review yield data, customer returns, and process logs regularly, making small adjustments that compound into meaningful gains. Together, these habits keep PPAL's quality standards climbing while keeping production efficient.
Contact Us
Contact Person: Nia
Email: [email protected]
Tel/WhatsApp: +86 18954360337
Website: https://www.sdppgi.com