Silicon Carbide Powder Vendor Evaluation Checklist for Buyers
2026-11-02
Buying silicon carbide powder usually starts with a datasheet and ends with surprises on the production line. That’s why we put together this vendor evaluation checklist—so you can separate dependable suppliers from the ones who just talk a good game. With input from HUAYI TECH, it covers the questions most buyers only think to ask after it’s too late.
Cutting Through Vendor Claims on SiC Powder Purity
Vendor data sheets often lead with a single number—99.99%, 99.999%, and occasionally even higher. What they rarely spell out is whether that figure covers only metallic impurities or includes oxygen, nitrogen, and carbon. A powder can hit five nines for metals yet still carry enough surface oxygen to ruin a MOSFET channel. Always ask which elements were measured, by what method, and on which sample lot.
The same purity claim means little without particle size and crystal structure context. A lot of fine, high-purity SiC powder may sinter beautifully but if the alpha/beta phase ratio is off, the resulting substrate warps or grows defects during PVT. Conversely, a slightly lower nominal purity with tightly controlled particle distribution often outperforms a “cleaner” powder that clumps or varies from batch to batch.
Smart buyers ignore the marketing number until they see batch-to-batch variation data and a third-party GDMS or SIMS report on actual impurity locations—surface versus lattice. If a vendor cannot provide that, the purity claim is just a sales slogan. Run your own small-scale sintering or crystal growth test with the exact furnace profile you plan to use, because only that will show whether the powder's impurity profile matters for your yield.
Why Particle Size Distribution Data Deserves a Second Look
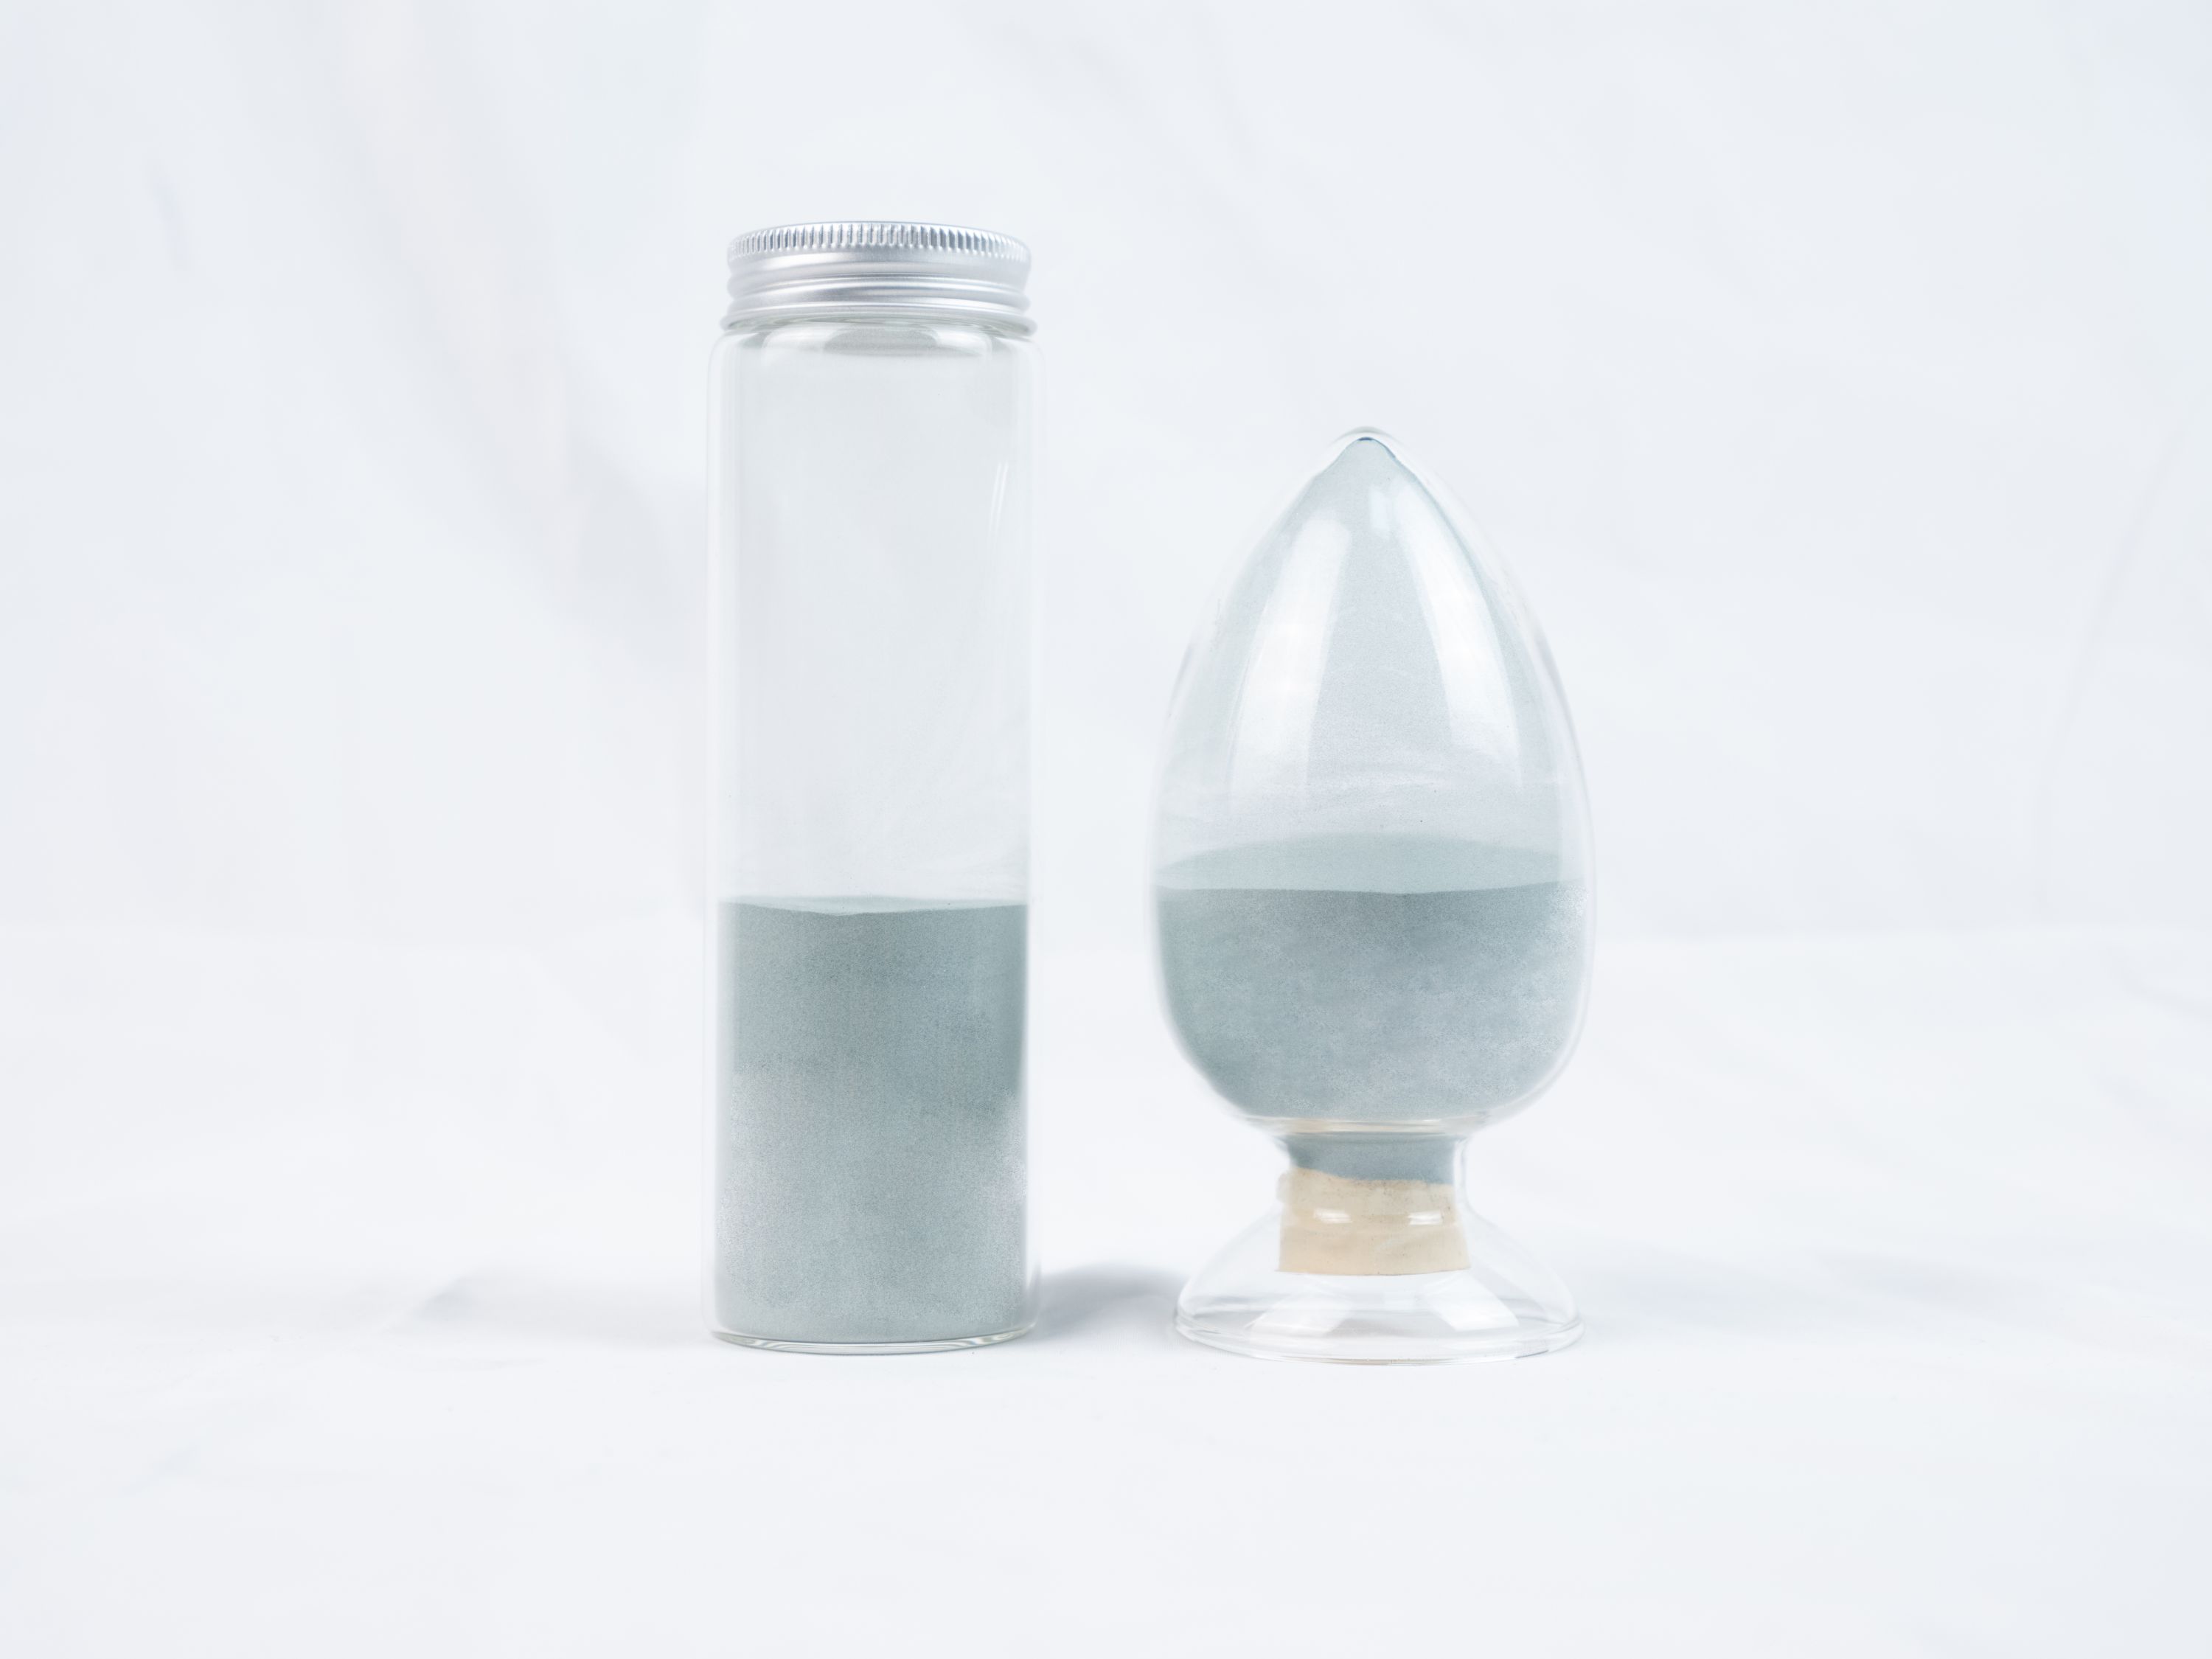
Most particle size reports get reduced to a single number—D50 or mean diameter—and the rest of the curve ends up as a footnote. That habit hides nearly all the useful information. A powder with the same D50 can pour like sand or clump like wet flour depending on whether the distribution is narrow, skewed, or split into two peaks. Skipping the shape of the distribution means ignoring exactly the features that decide how a material packs, flows, dissolves, or reacts.
When you reopen the full data, small shoulders and long tails stop being noise and start looking like evidence. A bimodal distribution might point to an unintended second nucleation event in crystallization, while a coarse tail can reveal a broken sieve or worn mill screen. These are not abstract statistics; they are fingerprints of real process upsets. Checking the raw histogram against previous batches often catches trouble before it becomes a rejected lot.
It also pays to look again because different techniques—laser diffraction, dynamic light scattering, sieve analysis—do not see the same sample the same way. Comparing only median values across methods can hide a mismatch that a full distribution overlay makes obvious. In coatings, battery slurries, and pharmaceutical blends, a shift in the fine fraction or the top 10% can change viscosity, settling, or bioavailability even when the median barely moves. That's why a second look at the whole curve is worth more than a fast glance at one summary statistic.
Red Flags in Batch Consistency That Cost You Later
The first sign usually shows up as a tiny variance between batches—maybe a shade off in color, a few milliseconds of delay, or a slightly different wording pattern. It’s easy to shrug off because the output still works. But those small drifts compound once you scale. What was a minor correction in a run of 50 becomes a full rework when you hit 5,000, and suddenly the cost isn’t just time—it’s the trust you lose when customers notice the inconsistency you overlooked.
Another red flag is the absence of a hard stop for out-of-spec batches. If your process lets every batch through as long as someone eyeballs it and says ‘close enough,’ you’re building a debt that comes due later. Without a clear acceptance threshold, borderline outputs pile up quietly. By the time the pattern is obvious, you’re not fixing a single batch—you’re auditing weeks of work and apologizing to stakeholders who expected a uniform result.
Watch for the moment when your consistency depends on one person’s memory or a spreadsheet that nobody updates. That’s not a process; it’s a ticking clock. When that person is out sick or the spreadsheet gets corrupted, the next batch drifts and nobody catches it until a client flags the mismatch. The fix is boring but effective: define the critical attributes for every batch, measure them the same way each time, and log the results before the batch ships. Skip that step and you’re not saving time—you’re just postponing a messier correction.
The Technical Support Gut Check Every Buyer Should Do
Most vendors will promise you the moon when it comes to support, but a gut check means putting their claims under real pressure before you sign. Skip the polished SLA slide and ask for the last three months of support ticket data—look at first response times for severity-one issues, not just averages. If they hesitate or hide behind "proprietary processes," that's your first red flag. Call their support line anonymously at 9 a.m. on a Tuesday and at 4:45 p.m. on a Friday. Time how long it takes to reach a human who can actually solve a problem, not just log it.
Then push on the escalation path: Who gets paged when your production database locks up at 2 a.m., and how many handoffs happen before an engineer with write access sees the ticket? Ask for a named support engineer or pod model rather than a generic queue. A strong vendor will walk you through a real incident postmortem—not the sanitized marketing version, but one with mistakes and fixes. Finally, check their community and documentation depth by picking an obscure error message and seeing if you can self-serve a solution in under five minutes. If the path to help is muddy now, it won't get clearer when you're down.
Traceability Audits: Questions That Expose Weak Suppliers
Most traceability audits fail before they begin because buyers ask the same predictable questions: 'Do you have a certificate?' or 'Can you share your supplier list?' Weak suppliers have rehearsed answers for these. Instead, start by asking for a live walk-through of one specific product's journey from raw material to finished good, on a randomly selected date. Ask to see the actual batch records, not the polished summary. If a supplier hesitates to open their production log or suddenly needs 'management approval' for a trivial detail, that's your first red flag.
Another line of questioning that separates robust operations from fragile ones is probing the 'what if' scenarios. Ask: 'If your primary dye supplier went offline tomorrow, how would you maintain color consistency for order #1123?' A capable supplier will walk you through their contingency stock, alternative source qualification, and re-testing protocol without blinking. A weak one will pivot to vague reassurances like 'we have many partners' or 'this never happens.' Follow up by requesting proof of a past disruption and how they recovered. No documented recovery, no real resilience.
Finally, test the internal handoffs. Ask the quality manager to explain how a defect found at final inspection gets traced back to a specific incoming lot. Then separately ask a warehouse operator the same question. If the two answers don't line up—if one describes a barcode-driven system while the other talks about manual stickers—you've uncovered a break in the chain that no polished audit report will mention. Strong suppliers train everyone to speak the same traceability language, not just the compliance officer.
Negotiating Price Without Inviting Quality Shortcuts
Driving down unit cost rarely happens in a vacuum. The moment a buyer signals that price is the deciding factor, some suppliers quietly recalculate how to preserve their margin. They might swap a certified raw material for a cheaper lookalike, reduce tolerance checks, or cut corners on finishing. What looks like a successful negotiation on paper can show up weeks later as higher defect rates, more returns, and a damaged brand. So the real challenge isn't just getting a lower number—it's making sure that number doesn't quietly shift the manufacturing floor's priorities.
One practical approach is to anchor the conversation in detailed specifications rather than vague expectations. Instead of saying "good quality," spell out the exact alloy grade, surface roughness, tensile strength, or acceptable blemish count. Then attach those specs to measurable acceptance criteria and make final payment contingent on inspection results. This turns quality from an emotional promise into a contractually enforceable baseline. Another lever is to talk about total cost of ownership, not just invoice price. If a supplier knows you are tracking rework hours, scrap rates, and warranty claims, they realize that cutting corners to hit a low bid will cost them future orders or trigger penalties. You can even offer a small volume commitment in exchange for holding quality standards—suppliers often accept a tighter margin when they can count on steady throughput.
Long-term relationships also change the risk calculus. A vendor who expects repeat business is less likely to gamble on substandard materials for a one-time win. Pair that expectation with unannounced audits or sample testing from each batch, and the incentive to shortcut quietly disappears. Likewise, invite the supplier to suggest cost-saving ideas that don't compromise integrity—like packaging optimization or delivery consolidation. This shifts the negotiation from a zero-sum price squeeze into a joint problem-solving exercise, where both sides can lower costs without lowering the bar.
FAQ
Start with the exact application the powder will serve. Ask for a batch certificate covering particle size distribution, major impurities, and crystal phase. If the vendor can't produce that certificate before a purchase commitment, the evaluation should end there.
D10, D50, and D90 values give the clearest picture of spread and central tendency. For demanding sintering or polishing work, also ask for BET surface area and a full particle size curve. A tight distribution with no bimodal peaks usually predicts more uniform microstructure in the final product.
Never rely on a marketing datasheet alone. Request a recent independent lab report or send a retained sample to a third-party lab for oxygen, free silicon, free carbon, and metallic impurities. Pay special attention to elements that harm your process, such as iron, aluminum, or calcium.
Consistency matters more than a single excellent batch. Ask for data from at least three consecutive production lots and compare the drift in D50, surface area, and impurity levels. Vendors with poor process control will show wider swings, which usually leads to unpredictable downstream yields.
Request a trial whenever switching suppliers or launching a new product line. A 25 kg or 50 kg trial run lets you test flowability, mixing behavior, and sintering response without tying up inventory. If a vendor refuses trials for serious buyers, treat that as a red flag.
A capable vendor should readily offer ISO or equivalent quality certificates, REACH or RoHS statements where relevant, safety data sheets, and full traceability from raw material lot to finished powder batch. Missing traceability or vague origin claims often hide inconsistent sourcing.
Convert quotes to cost per usable kilogram, not per ton. Factor in scrap rate, rework caused by batch variation, and logistics reliability. A powder that looks cheap but causes a 5% yield loss will quickly erase its price advantage against a stable, slightly more expensive supply.
Watch for unwillingness to share batch data, sudden changes in origin without notice, vague answers about contamination control, and persistent delivery delays. Also be cautious when a vendor cannot explain how they prevent cross-contamination between different grit sizes or product grades.
Conclusion
When evaluating silicon carbide powder suppliers, dig past the polished marketing sheets. Purity percentages sound impressive until you ask for the actual test method—was it bulk chemistry or surface-sensitive? If a vendor can't produce raw data from multiple lots, treat the number as provisional. Particle size distribution deserves the same skepticism. A single average value hides tails that can wreck sintering behavior or packing density. Request full distribution curves, not just D50, and compare them across production runs. Batch-to-batch drift often shows up first in the fine fraction, so watch for shifts that look minor on paper but will change your downstream process.
Technical support is another quiet differentiator. Call the vendor with a realistic processing problem before signing anything—if you get routed to sales instead of an engineer, that's your answer. Traceability should extend beyond a certificate of origin; ask how they link each lot to raw material sources, furnace runs, and milling parameters. Weak suppliers stumble when you ask for deviation records or out-of-spec dispositions. Finally, negotiate price on total cost of ownership, not per-kilogram sticker. A cheaper powder that forces extra screening, longer milling, or higher scrap rates is no bargain. Lock down quality metrics in the purchase agreement, and make clear that unannounced specification changes will void the contract. Buyers who push on these points early end up with fewer surprises and a supplier that treats consistency as a default, not a request.
Contact Us
Contact Person: Junting Leo
Email: [email protected]
Tel/WhatsApp: +86 18615009766
Website: https://www.huayimaterial-china.com/